GSS Bulk Material Handling Solution: Empowering JAPFA’s Feed Supply Chain Expansion in Indonesia
Key Highlights
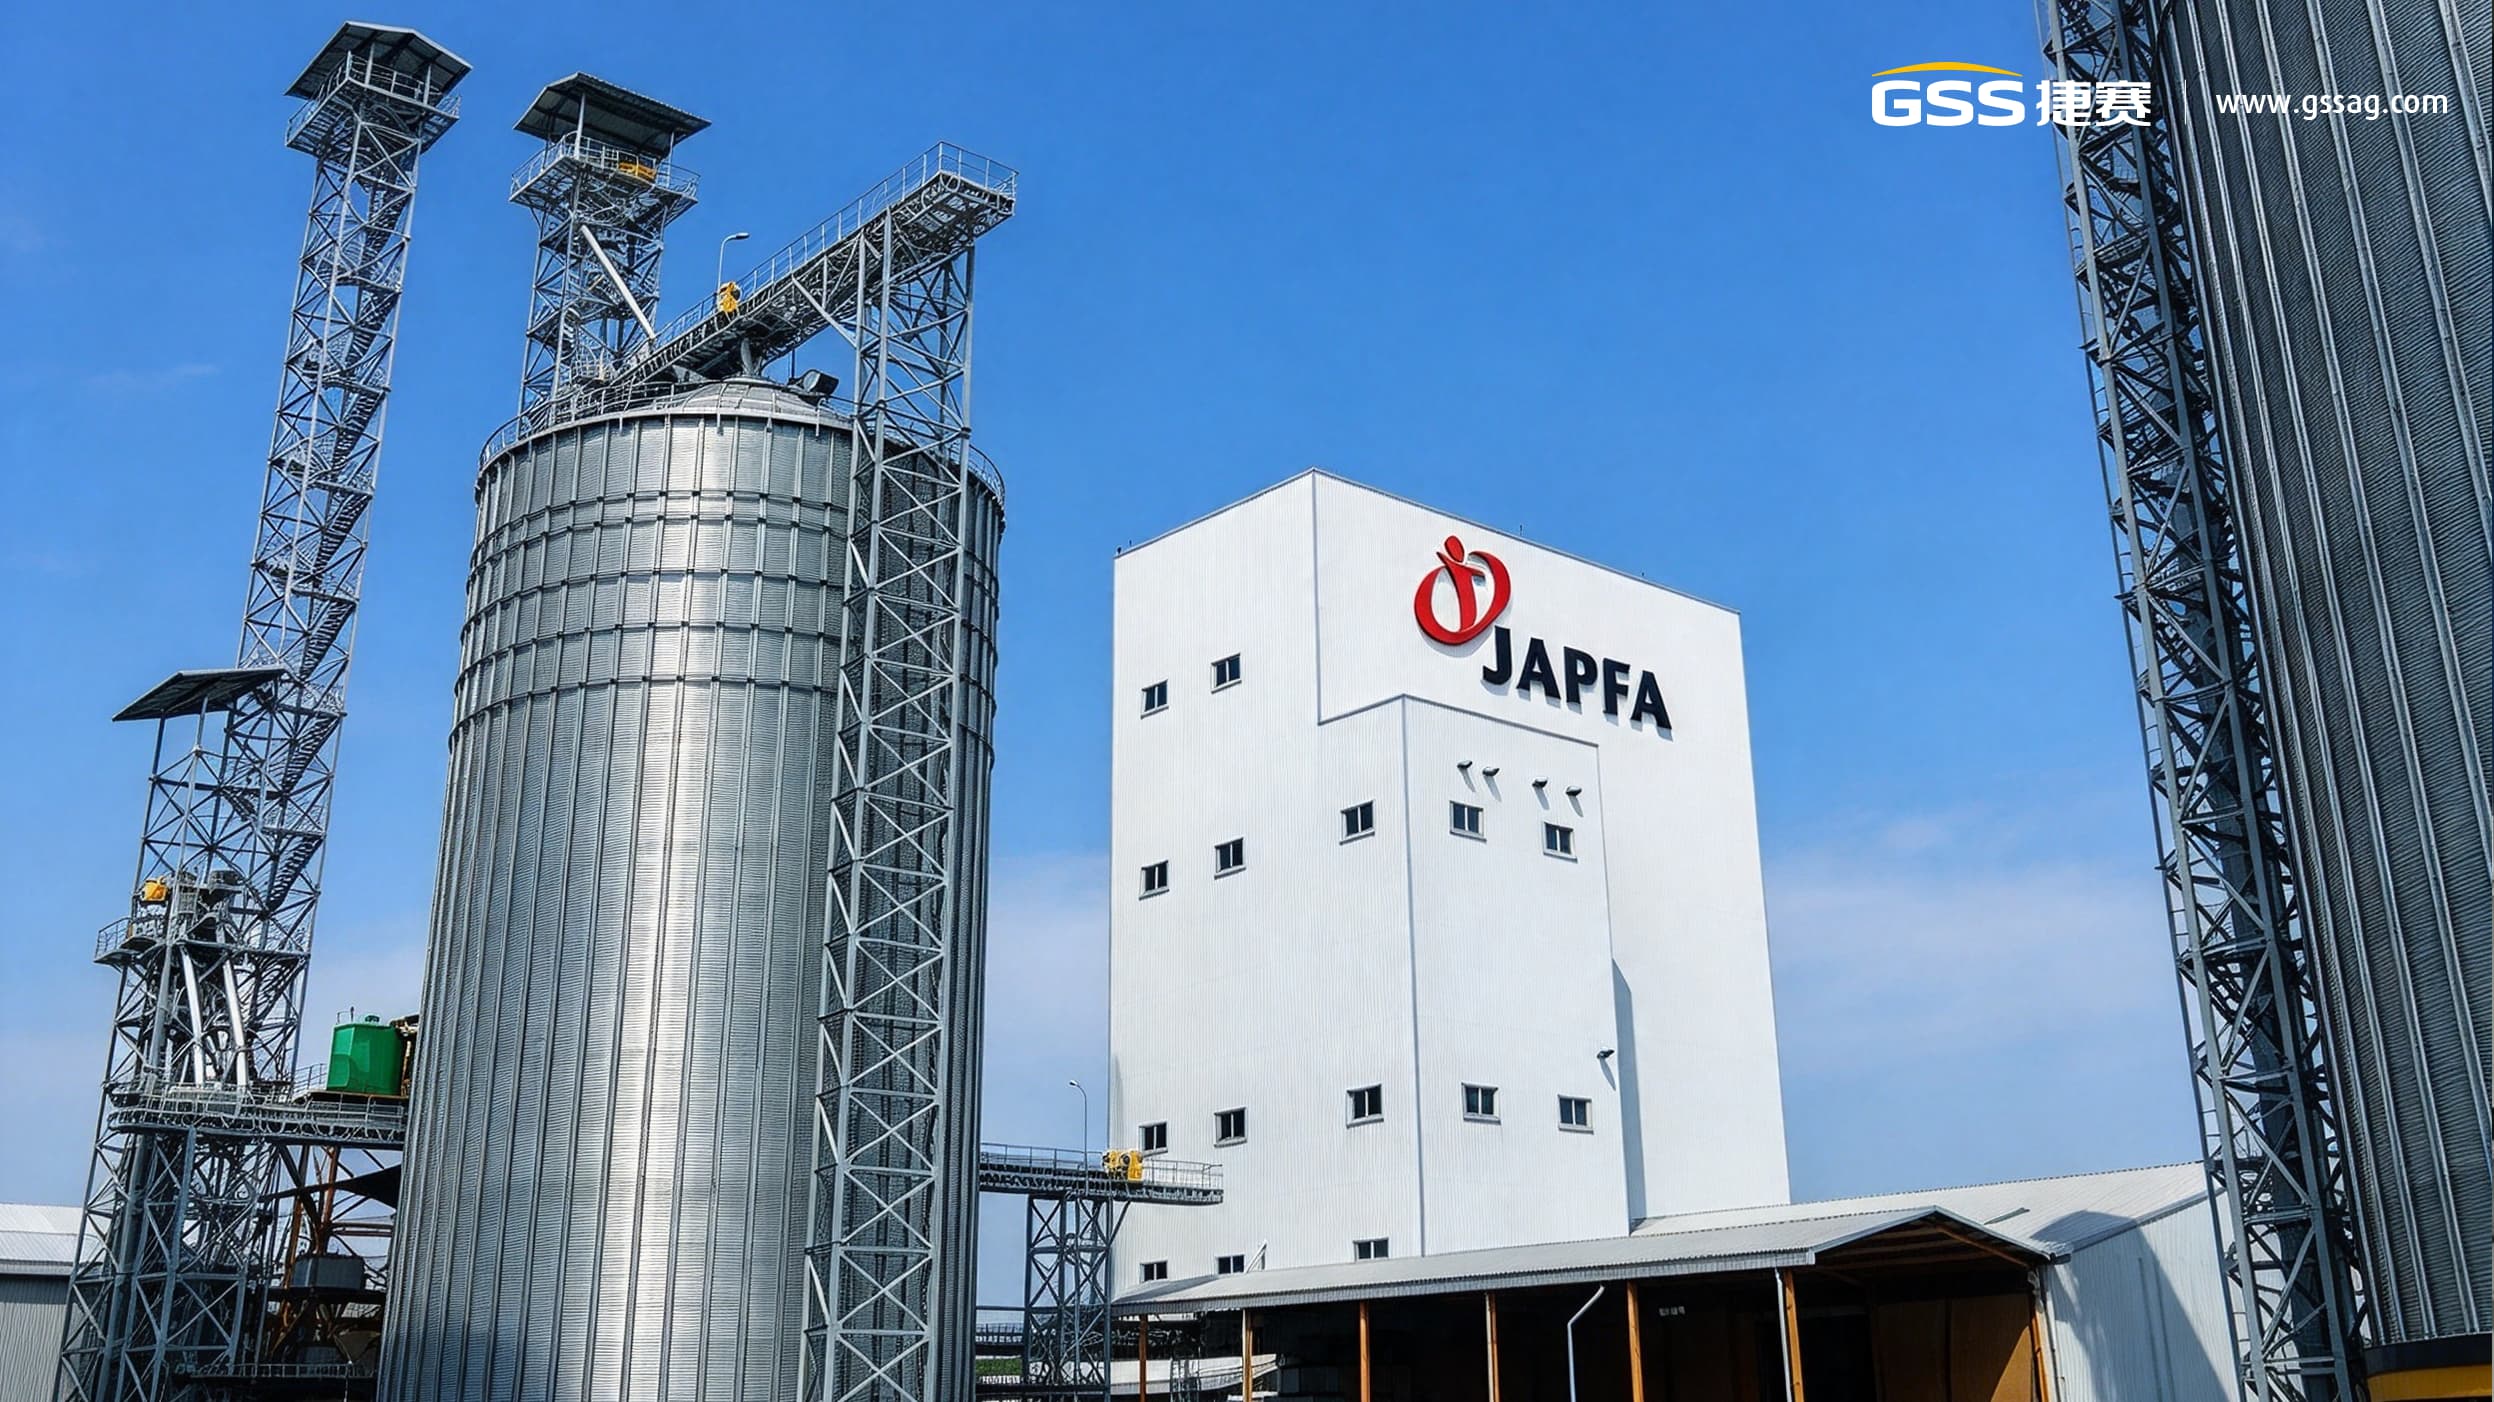
PT. JAPFA COMFEED INDONESIA Tbk launched a major expansion project at its Bati2 plant to upgrade the handling, storage, and processing supply systems for raw corn, resolving logistics bottlenecks and bolstering finished feed storage and dispatch capabilities.
Deployed a customized, highly sealed, and corrosion-resistant GSS bulk material handling and flow control system, consisting of 5 sets of high-capacity En-Masse Conveyors and precision Slide Gate Valves engineered for tropical high-humidity environments and continuous duty operations.
Achieved major breakthroughs in low-breakage grain transfer, zero-dust green operations, and automated precision material control, ensuring uninterrupted production and establishing a flagship supply chain benchmark in Indonesia.
Client Profile: A Leading Agri-Food Company in Southeast Asia
JAPFA COMFEED INDONESIA Tbk (JAPFA Group) is a leading agri-food company in Southeast Asia, holding a dominant market position in poultry farming, feed production, and aquaculture in Indonesia.
Driven by rising regional demand for high-quality poultry and animal feed, JAPFA initiated the expansion of its Bati2 feed mill. Centered on upgrading raw corn bulk handling and workshop dosing systems, this expansion serves as a landmark strategic initiative to bolster feed supply chain resilience and operational efficiency.
Goals & Challenges
To meet the continuous, large-scale production demands, the JAPFA project team faced three universal industry challenges stemming from tropical operating conditions and intensive industrial manufacturing:
- Equipment Reliability under Tropical Extremes: Indonesia’s tropical climate brings high temperatures and extreme humidity. Combined with raw corn containing varying impurities and particle sizes, conventional conveyors suffer from corrosion, chain wear, and mechanical jams, threatening costly downtime.
- Grain Integrity & Dust Emission Control in Bulk Transfer: High-speed conveying and drop heights during bin top distribution and dosing cause grain damage and generate airborne dust. Dust leads to material loss, strict environmental compliance issues, and severe combustible dust explosion hazards.
- Automated Precision Flow Control for Multi-Silo Systems: Expanding storage capacity required dynamic switching and precise flow shut-off across multiple silos and production lines. Conventional valves often leak or jam, hindering automated and refined material management.
Customized Solution:High-Reliability Continuous Conveying & Precision Flow Control System Under Severe Conditions
Engineered for severe tropical conditions and stringent operational standards, GSS delivered a customized bulk handling solution integrating anti-corrosion durability, gentle dust-tight conveying, and precision flow control:
- En-Masse Conveyors (5 units):Handling 100 MT/H each across lengths from 13.2m to 26.2m (inclines 0°-3°), these units feature enhanced anti-corrosion coatings and wear-resistant liners on headstocks, tails, and casings to withstand tropical humidity and abrasive impurities. The optimized flight structure pushes grain smoothly in bulk columns to minimize kernel damage, while the fully enclosed design prevents dust leakage, meeting strict environmental and explosion-proof standards.
- Slide Gate Valves (2 units):Designed for high-capacity flow cut-off and diverting. Equipped with self-cleaning seal technology and precise driving mechanisms, these valves guarantee zero leakage and anti-jamming performance during high-volume material handling, ensuring exceptional reliability and easy maintenance.
Project Value
High Logistics Capacity
The high-capacity 100 MT/H bulk system operates continuously without bottlenecks, ensuring steady raw corn transfer and silo distribution to support the plant's upgraded processing targets.
Tropical Anti-Corrosion & Quality Preservation
Enhanced anti-corrosion/wear resistance and gentle, dust-tight conveying withstand tropical humidity and abrasive impurities while minimizing kernel breakage to preserve grain quality.
Automated Control & Continuous Operational Stability
Seamlessly integrated automated valves facilitate dynamic flow routing and rapid cut-off. Low maintenance demands and reliable mechanical design guarantee smooth 24/7 continuous feed manufacturing.
“In our Bati2 plant expansion, ensuring a seamless and dust-free bulk raw corn handling system was crucial for our feed production continuity. GSS provided exceptional En-Masse Conveyors and precision valves tailored to South East Asia’s demanding tropical climate. The robust equipment design, zero dust leakage, and outstanding reliability have significantly boosted our supply chain efficiency, proving GSS to be a trusted partner in our growth.”