Smart Material Handling Solution: Empowering Shede Spirits in Ecological Brewing Modernized Upgrades
Key Highlights
Facing the demands of green development and high-end liquor quality, Shede Spirits Co., Ltd. (a core subsidiary of Sichuan Tuopai Shede Group) initiated a comprehensive modernization upgrade for its brewing preparation center, focusing on the automated, clean, and high-efficiency handling of rice husks, a critical auxiliary material for Chinese Baijiu solid-state fermentation.
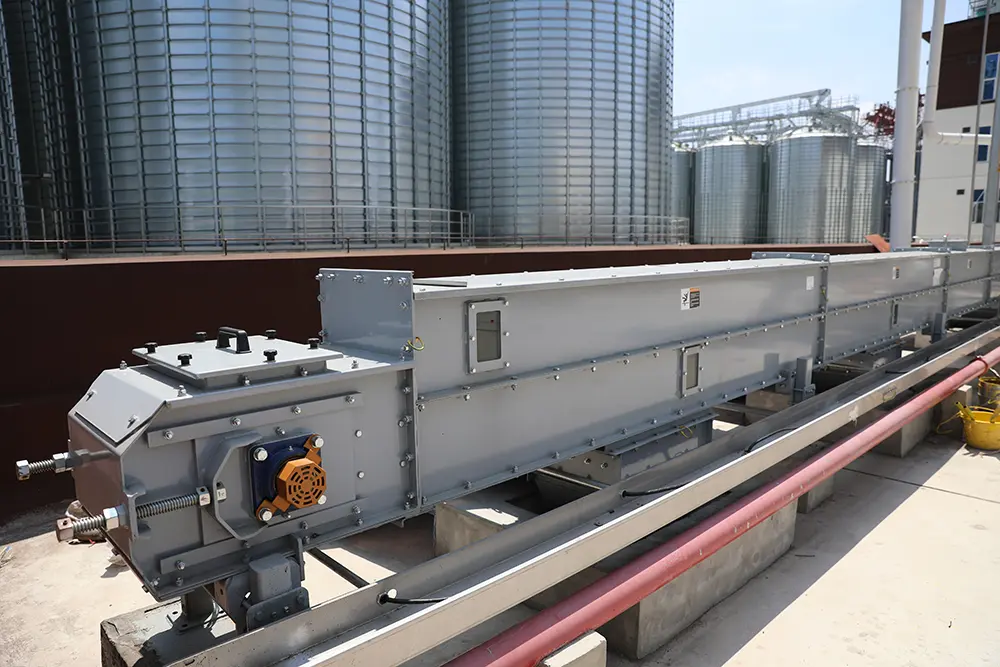
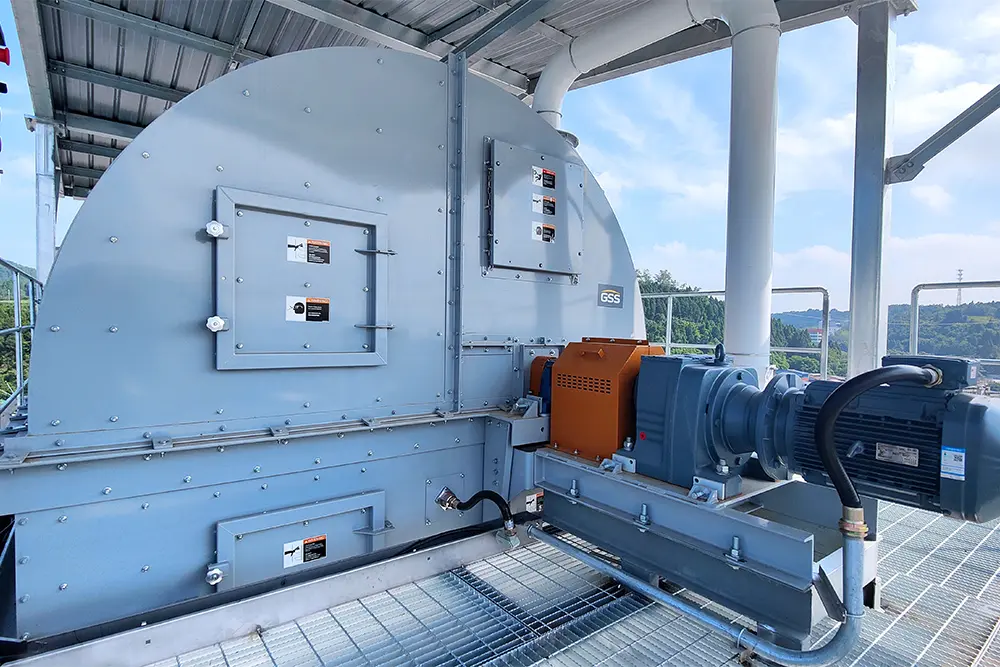
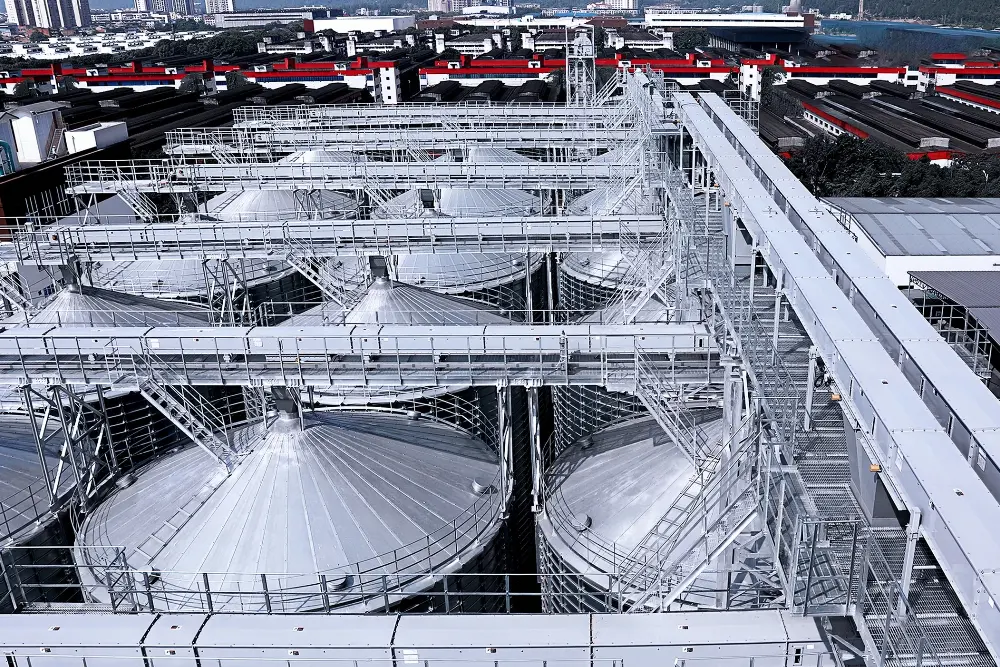
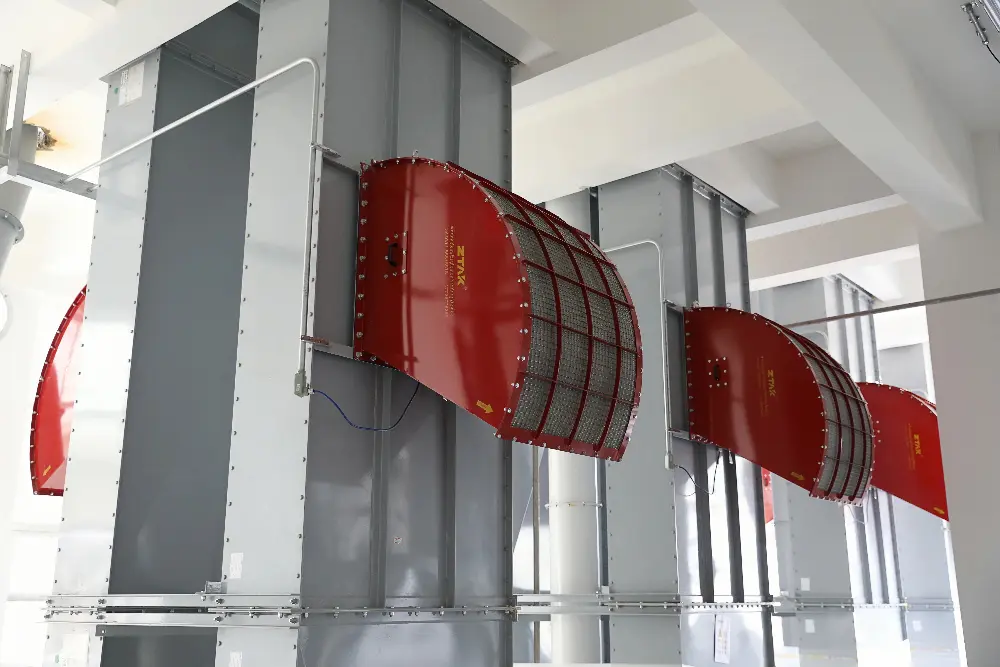
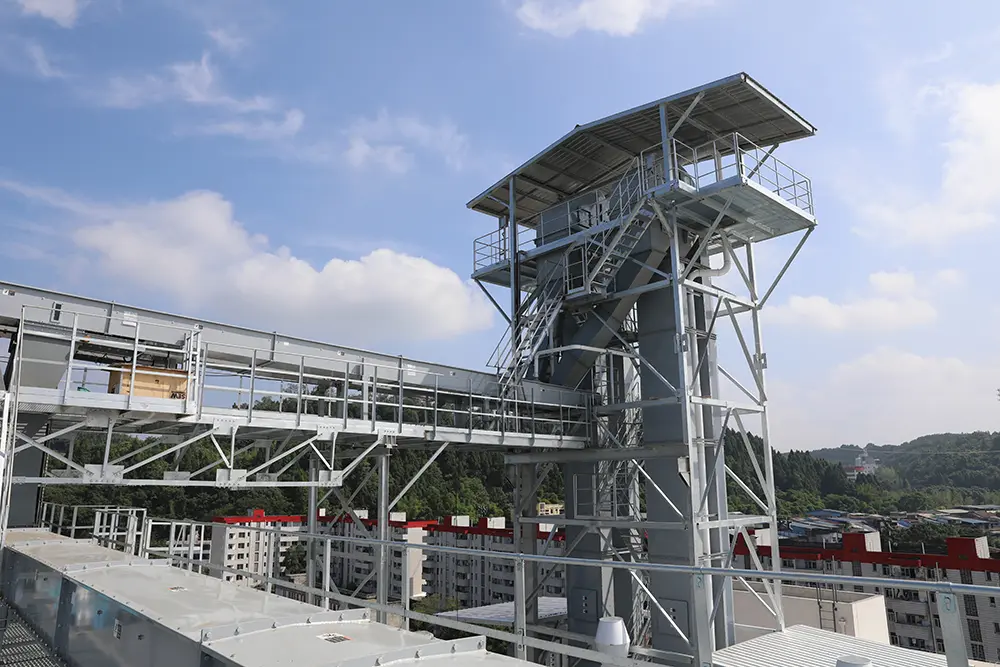
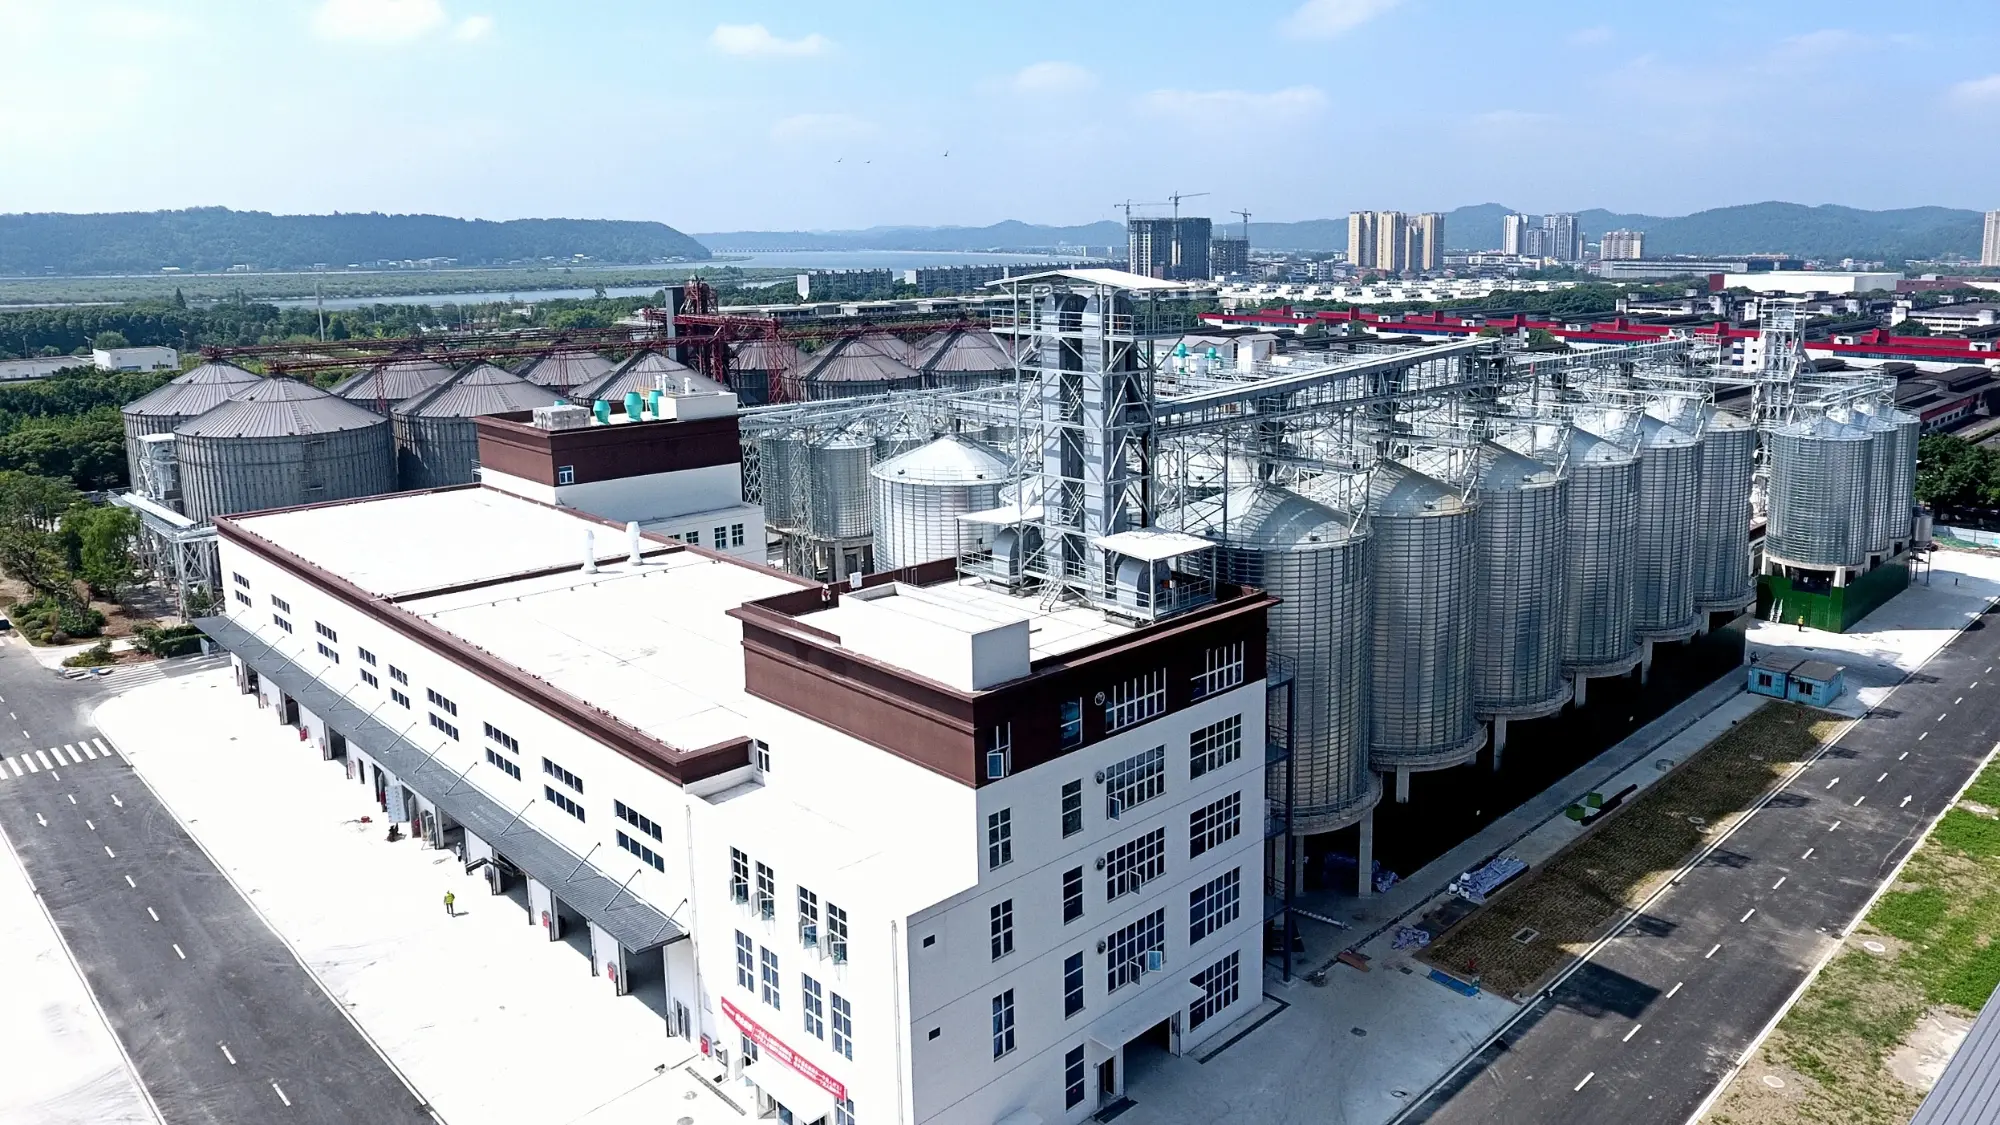
GSS engineered and delivered a fully enclosed, automated turnkey solution covering rice husk unloading, magnetic separation, high-efficiency screening, precise metering, silo storage, continuous steaming & cooling, and automated palletizing/bagging systems, featuring robust equipment configurations like En-Masse Conveyors, Bucket Elevators, and specialized dust collection setups.
By deploying GSS’s fully automated, airtight material handling and continuous steaming system, Shede Spirits achieved a 100% capacity increase with a daily processing capacity of 280 metric tons, while drastically reducing manual labor and operational intensity.
Client Profile: a Prominent Leader in the Chinese Baijiu Industry and a Pioneer in Eco-Friendly Brewing
Headquartered in Suining, Sichuan Province, Shede Spirits Co., Ltd., backed by Sichuan Tuopai Shede Group, is a prominent leader in the Chinese Baijiu industry and a pioneer in eco-friendly brewing. Shede has long integrated natural ecological preservation into every step of its production.
In its continuous drive toward smart, automated, green, and intensive upgrades within its brewing preparation center, Shede identified the pretreatment of rice husks (Paddy husk/Rice hull)—an indispensable loosening agent used in solid-state fermentation mud pits—as a vital strategic link. The modernization of this segment directly dictates grain permeability, fermentation efficiency, and the ultimate aromatic profile of the liquor.
Goals & Challenges: Overcoming Efficiency Bottlenecks, Impurity Risks, and Dust Issues in Traditional Operations
In upgrading its traditional auxiliary material workflow, Shede Spirits faced three universal industry challenges in heavy-duty industrial brewing:
- Labor-Intensive & Low-Efficiency Handling: Traditional rice husk handling relied heavily on manual bagging, open transport, and disjointed handling, resulting in low throughput, heavy physical labor intensity, and bottlenecks failing to match modern high-capacity brewing schedules (280mt/day steaming requirement).
- Impurities & Quality Risks: Raw rice husks often contain field impurities, dust, and stray metallic shards. Unrefined processing risks introducing foreign odors, silicates, or metallic contaminants into the fermentation pits, directly threatening the exceptional flavor and purity of high-end liquor.
- Dust Pollution & Environmental Compliance: Open-air handling and traditional transfer of lightweight, bulky rice husks easily trigger severe dust pollution in the workshop, challenging strict environmental protection standards and modern clean-production mandates.
Customized Solution: Building a Full-Process Airtight, Automated, and Digital Turnkey System
Leveraging extensive industry expertise in bulk material handling, GSS tailored an integrated, closed-loop processing system for Shede Spirits. The comprehensive turnkey solution spans the entire lifecycle from raw material intake to final bagging and palletizing:
- Primary Unloading & Pre-Cleaning Line: Equipped with heavy-duty Under-Track Hoppers, Unpacking Machines, En-Masse Conveyors, and high-reliability Bucket Elevators to ensure smooth, continuous horizontal and vertical lifting of raw materials.
- Screening & Magnetic Separation System: Integrated multi-unit Cleaning Sieves, Magnetic Separators, and Flow Meters to systematically screen out physical impurities and extract metallic foreign objects, ensuring absolute husk purity.
- Advanced Storage & Buffer Network: Configured with specialized Storage Bins, Level Sensors, and Pneumatic/Manual Gates for seamless material routing, precise inventory control, and first-in-first-out (FIFO) management.
Project Value: Achieving Capacity Double, Quality Safeguards, and Green Production Benchmark
100% Capacity Growth & Operational Efficiency
Achieving a daily rice husk steaming capacity of 280 metric tons, the automated flow eliminated manual handling bottlenecks, slashed labor costs, and supercharged overall plant throughput.
Purity Enhancement & Flavor Safeguarding
Through multi-stage physical screening, magnetic clearance, and precision-controlled continuous steaming, volatile impurities and off-flavors were thoroughly purged, protecting the pristine quality and distinct sensory elegance of Shede's spirits.
Green, Airtight & Digital Workshop Benchmark
The full-process airtight mechanical design eradicated workshop dust emissions, while digital online flow meters and level sensors enabled data tracking, transforming a traditional auxiliary process into a modern, eco-friendly benchmark.
"Traditional brewing requires reverence for nature and extreme rigor in every fine detail. GSS helped us break the bottleneck between traditional craft and modern engineering. Their intelligent, fully enclosed rice husk processing system not only doubled our capacity and reduced labor intensity, but more importantly, ensured the absolute purity of our brewing raw materials. It is a powerful technical engine driving Shede's ecological brewing strategy forward."