Enclosed Tubular Conveying System: Empowering Ronsy Pet Food for High-Hygiene & Low-Breakage Ingredient Handling
Key Highlights
In response to stringent requirements for "zero breakage, zero residue, and high cleanliness" in premium pet food raw material handling, Ronsy Pet Food Co., Ltd. partnered with GSS to comprehensively upgrade its legacy conveying processes.
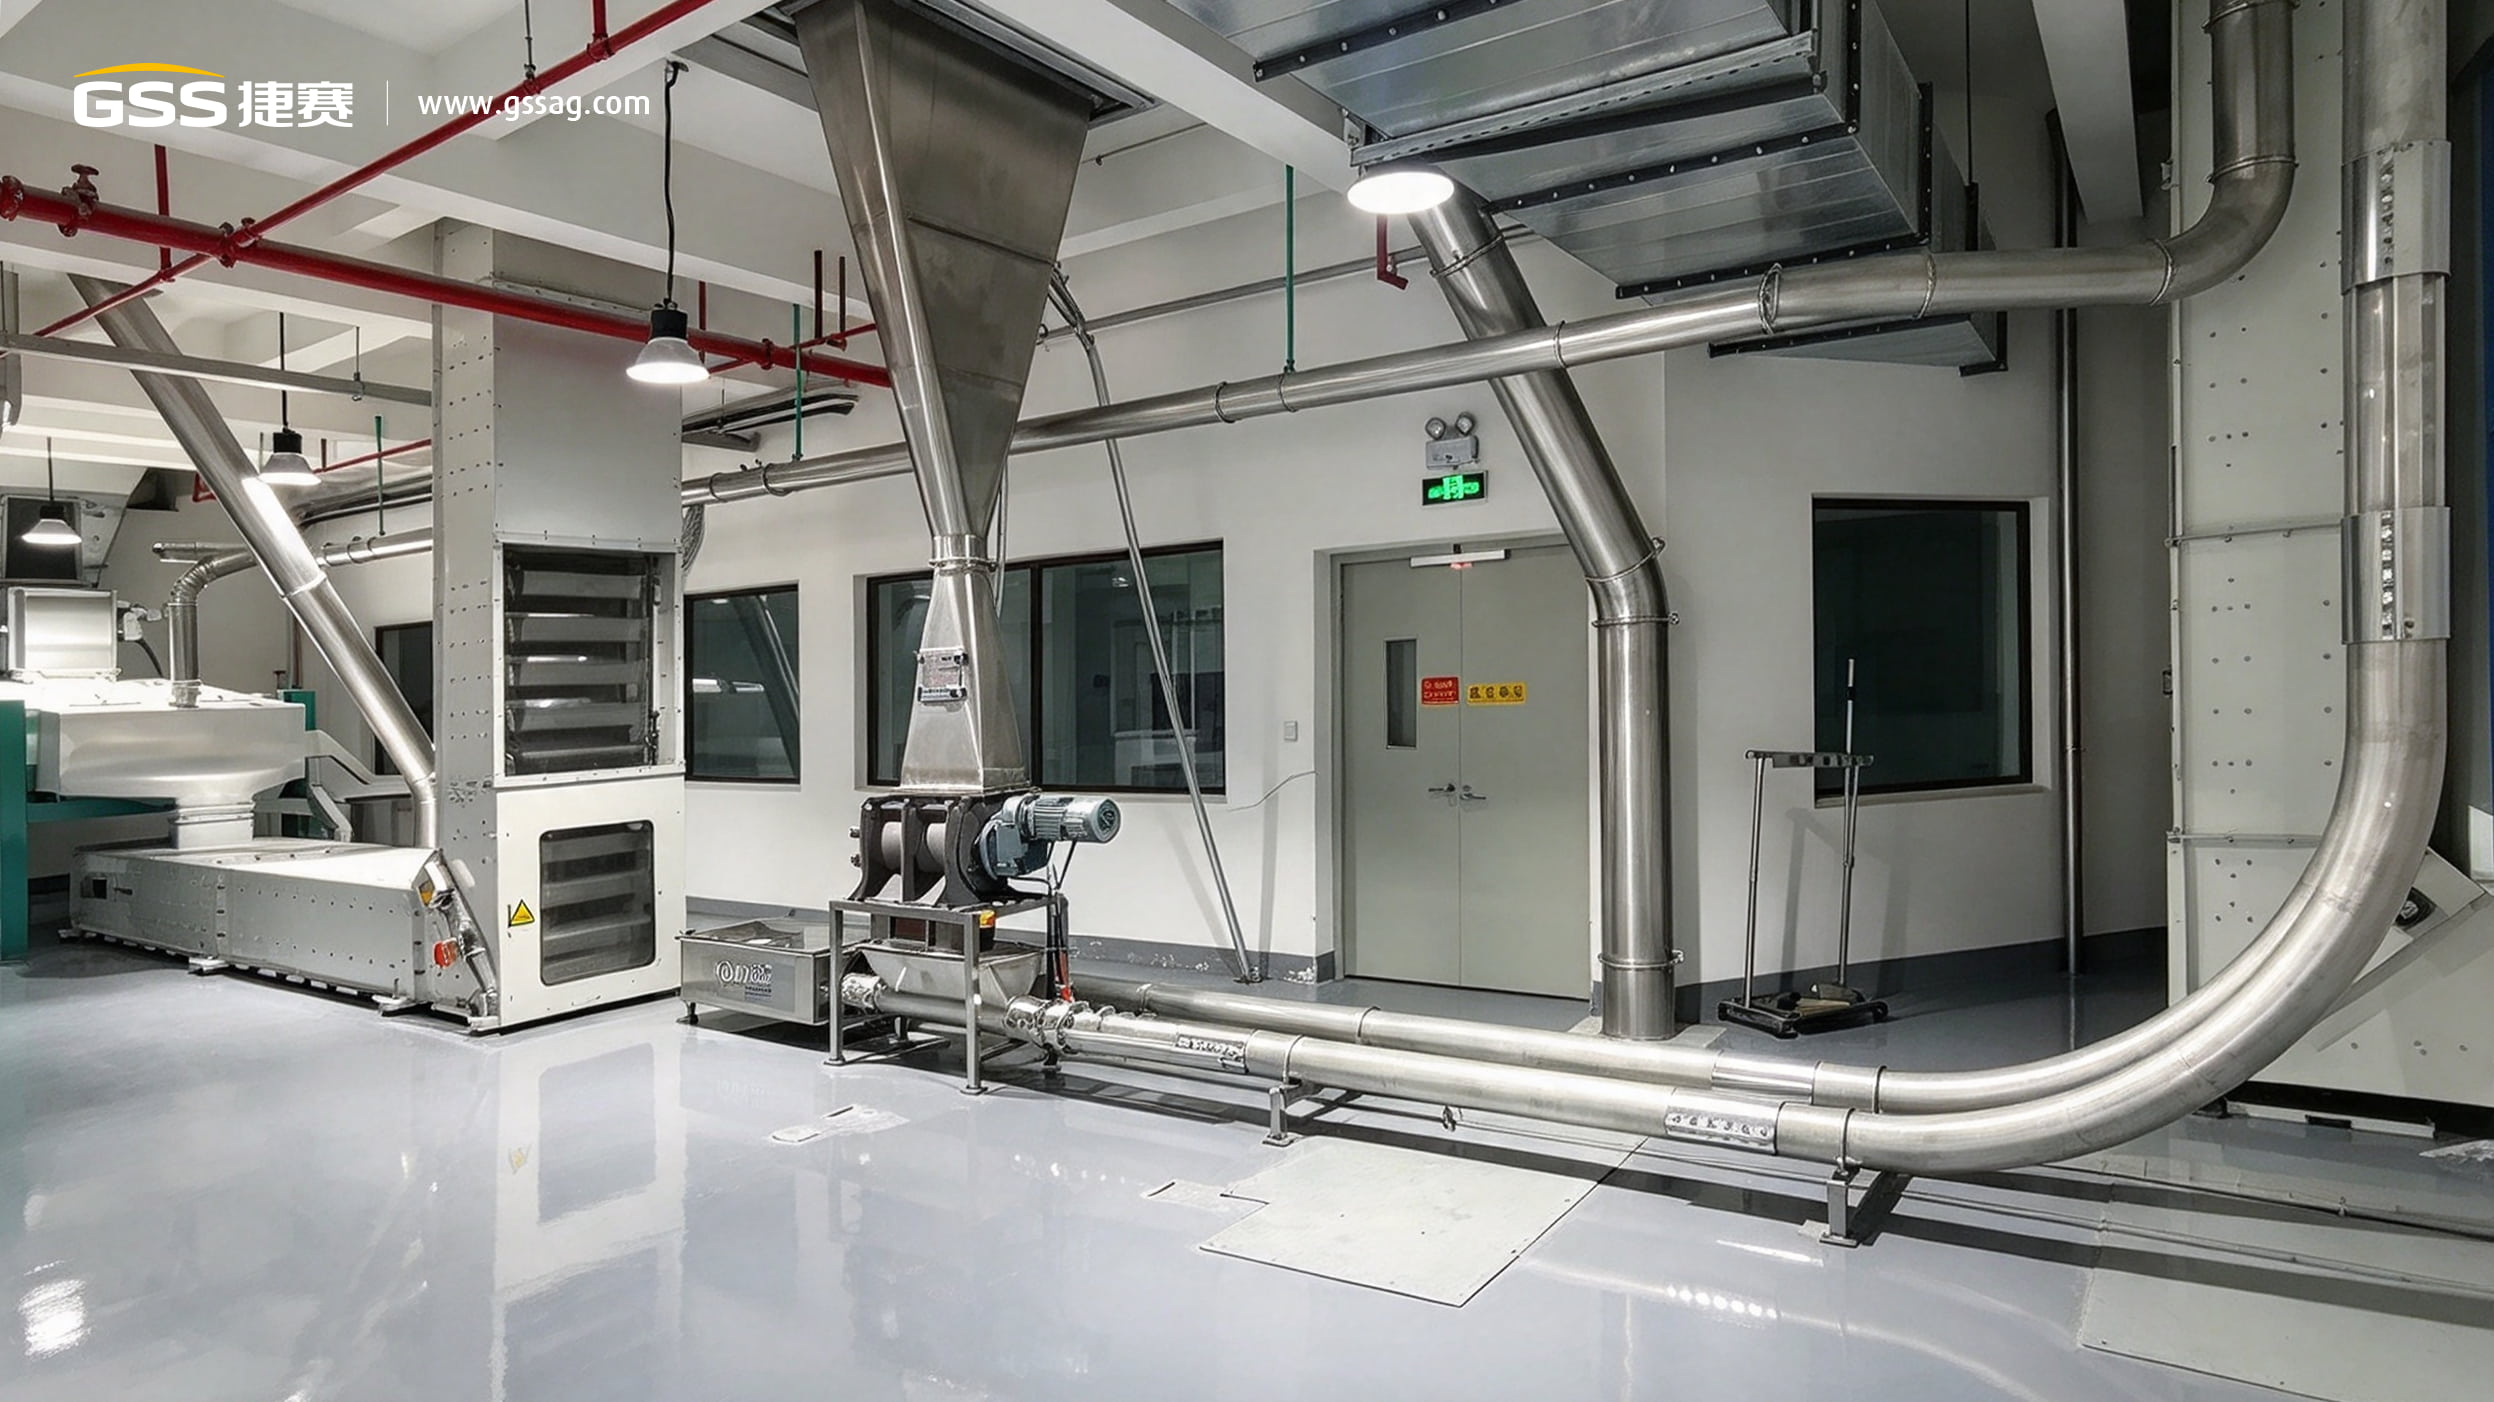
Deployed a customized equipment suite centered around high-precision Chain and Disc Conveyors and enclosed tubular conveying lines, ensuring gentle and efficient flow of pet food ingredients within a fully sealed environment.
Achieved three core benefits: "low material loss, high production hygiene, and simplified maintenance," significantly enhancing Ronsy's core competitiveness in the premium pet food supply chain.
Client Profile: A Leading High-End Pet Food Enterprise in China
Hebei Ronsy Pet Food Co., Ltd. is a leading enterprise in China’s premium pet food manufacturing sector, holding a prominent market position in the refined R&D and large-scale production of dry food, wet food, and specialized diet formulas.
Driven by surging domestic and international demand for high-quality and safe pet food, the company initiated a key expansion project at its modern Xingtai production facility. Centered on upgrading pet food ingredient handling via fully enclosed, low-breakage conveying and dust-free hygienic systems, this upgrade serves as a landmark strategic initiative to bolster brand positioning, supply chain resilience, and product safety.
Goals & Challenges
During the initial planning phase, the project management team at Ronsy Pet Food faced key technical bottlenecks common in the pet food industry that directly impacted end-product quality and food safety:
- Equipment Hygiene & Microbial Control: Pet food ingredients (such as extruded pellets, grain meals, and formulation powders) demand exceptionally high hygiene standards. Conventional conveyors feature internal dead zones and dust accumulation, creating breeding grounds for mold and microbes that fall short of strict food safety compliance.
- Ingredient Integrity & Breakage Reduction: Pet food pellets and sensitive raw ingredients are vulnerable to breakage and degradation caused by harsh impacts and friction during traditional mechanical conveying. This damages formulation accuracy, degrades product appearance, and directly reduces premium market value.
- Zero-Residue & Rapid Cleaning for Multi-Recipe Lines: Upgrading production lines required frequent recipe changes across various pet food product lines. Conventional conveying equipment is difficult to clean and prone to residual buildup, risking cross-contamination between batches and hindering operational efficiency.
Customized Solution: Fully Enclosed Gentle Tubular Conveying & Clean-System Deployment
Tailored to the process characteristics and stringent hygiene standards of Ronsy Pet Food, the GSS engineering team delivered a comprehensive equipment solution encompassing mainline conveying, quality protection, and smart cleaning systems:
- Core Tubular Conveying Mainline: Deployed multiple high-precision Chain and Disc Conveyors and enclosed tubular conveying lines. Utilizing disc flights pulled by a flexible circuit inside closed tubes, the system enables continuous and steady 3D movement (horizontal, inclined, or vertical) for pet food ingredients.
- Gentle Handling & Zero-Dead-Zone Design: The gentle conveying motion moves materials in a relatively static state within the pipe, minimizing breakage at the source. The precision-engineered pipeline features zero internal dead zones, completely preventing external dust contamination and material leakage.
- Food-Grade Cleanliness & Rapid Maintenance: Built with wear-resistant, easy-to-clean food-grade materials and paired with modular quick-release maintenance ports, the system maintains superior internal hygiene, significantly reduces microbial risks, and supports seamless recipe switchovers.
Project Value
Low Breakage & Premium Market Value
The system preserves the physical integrity of pet food pellets and raw ingredients, drastically reducing breakage and degradation while directly boosting end-product appearance and premium market value.
Continuous Capacity & Clean Logistics
Fully enclosed tubular conveying completely eliminates airborne dust and residual buildup, creating a clean, dust-free logistics artery that ensures uninterrupted, high-capacity plant operations.
Hygienic Safety & Reduced Maintenance Costs
The food-grade, highly hygienic conveying environment fundamentally cuts the risk of microbial cross-contamination. Robust machinery with low-maintenance requirements significantly reduces total operational costs.
"GSS provided us with a closed tubular conveying system that completely resolved our long-standing challenges regarding raw material breakage and workshop hygiene. The system operates with exceptional stability and low energy consumption, while achieving industry-leading standards in material quality protection and food safety. GSS's professional engineering capabilities and reliable technological empowerment have laid a solid foundation for us to build a high-end pet food brand."