High-Capacity Drying & Handling System | Yihai Kerry East China 700,000TPY Rice Base
Key Highlights
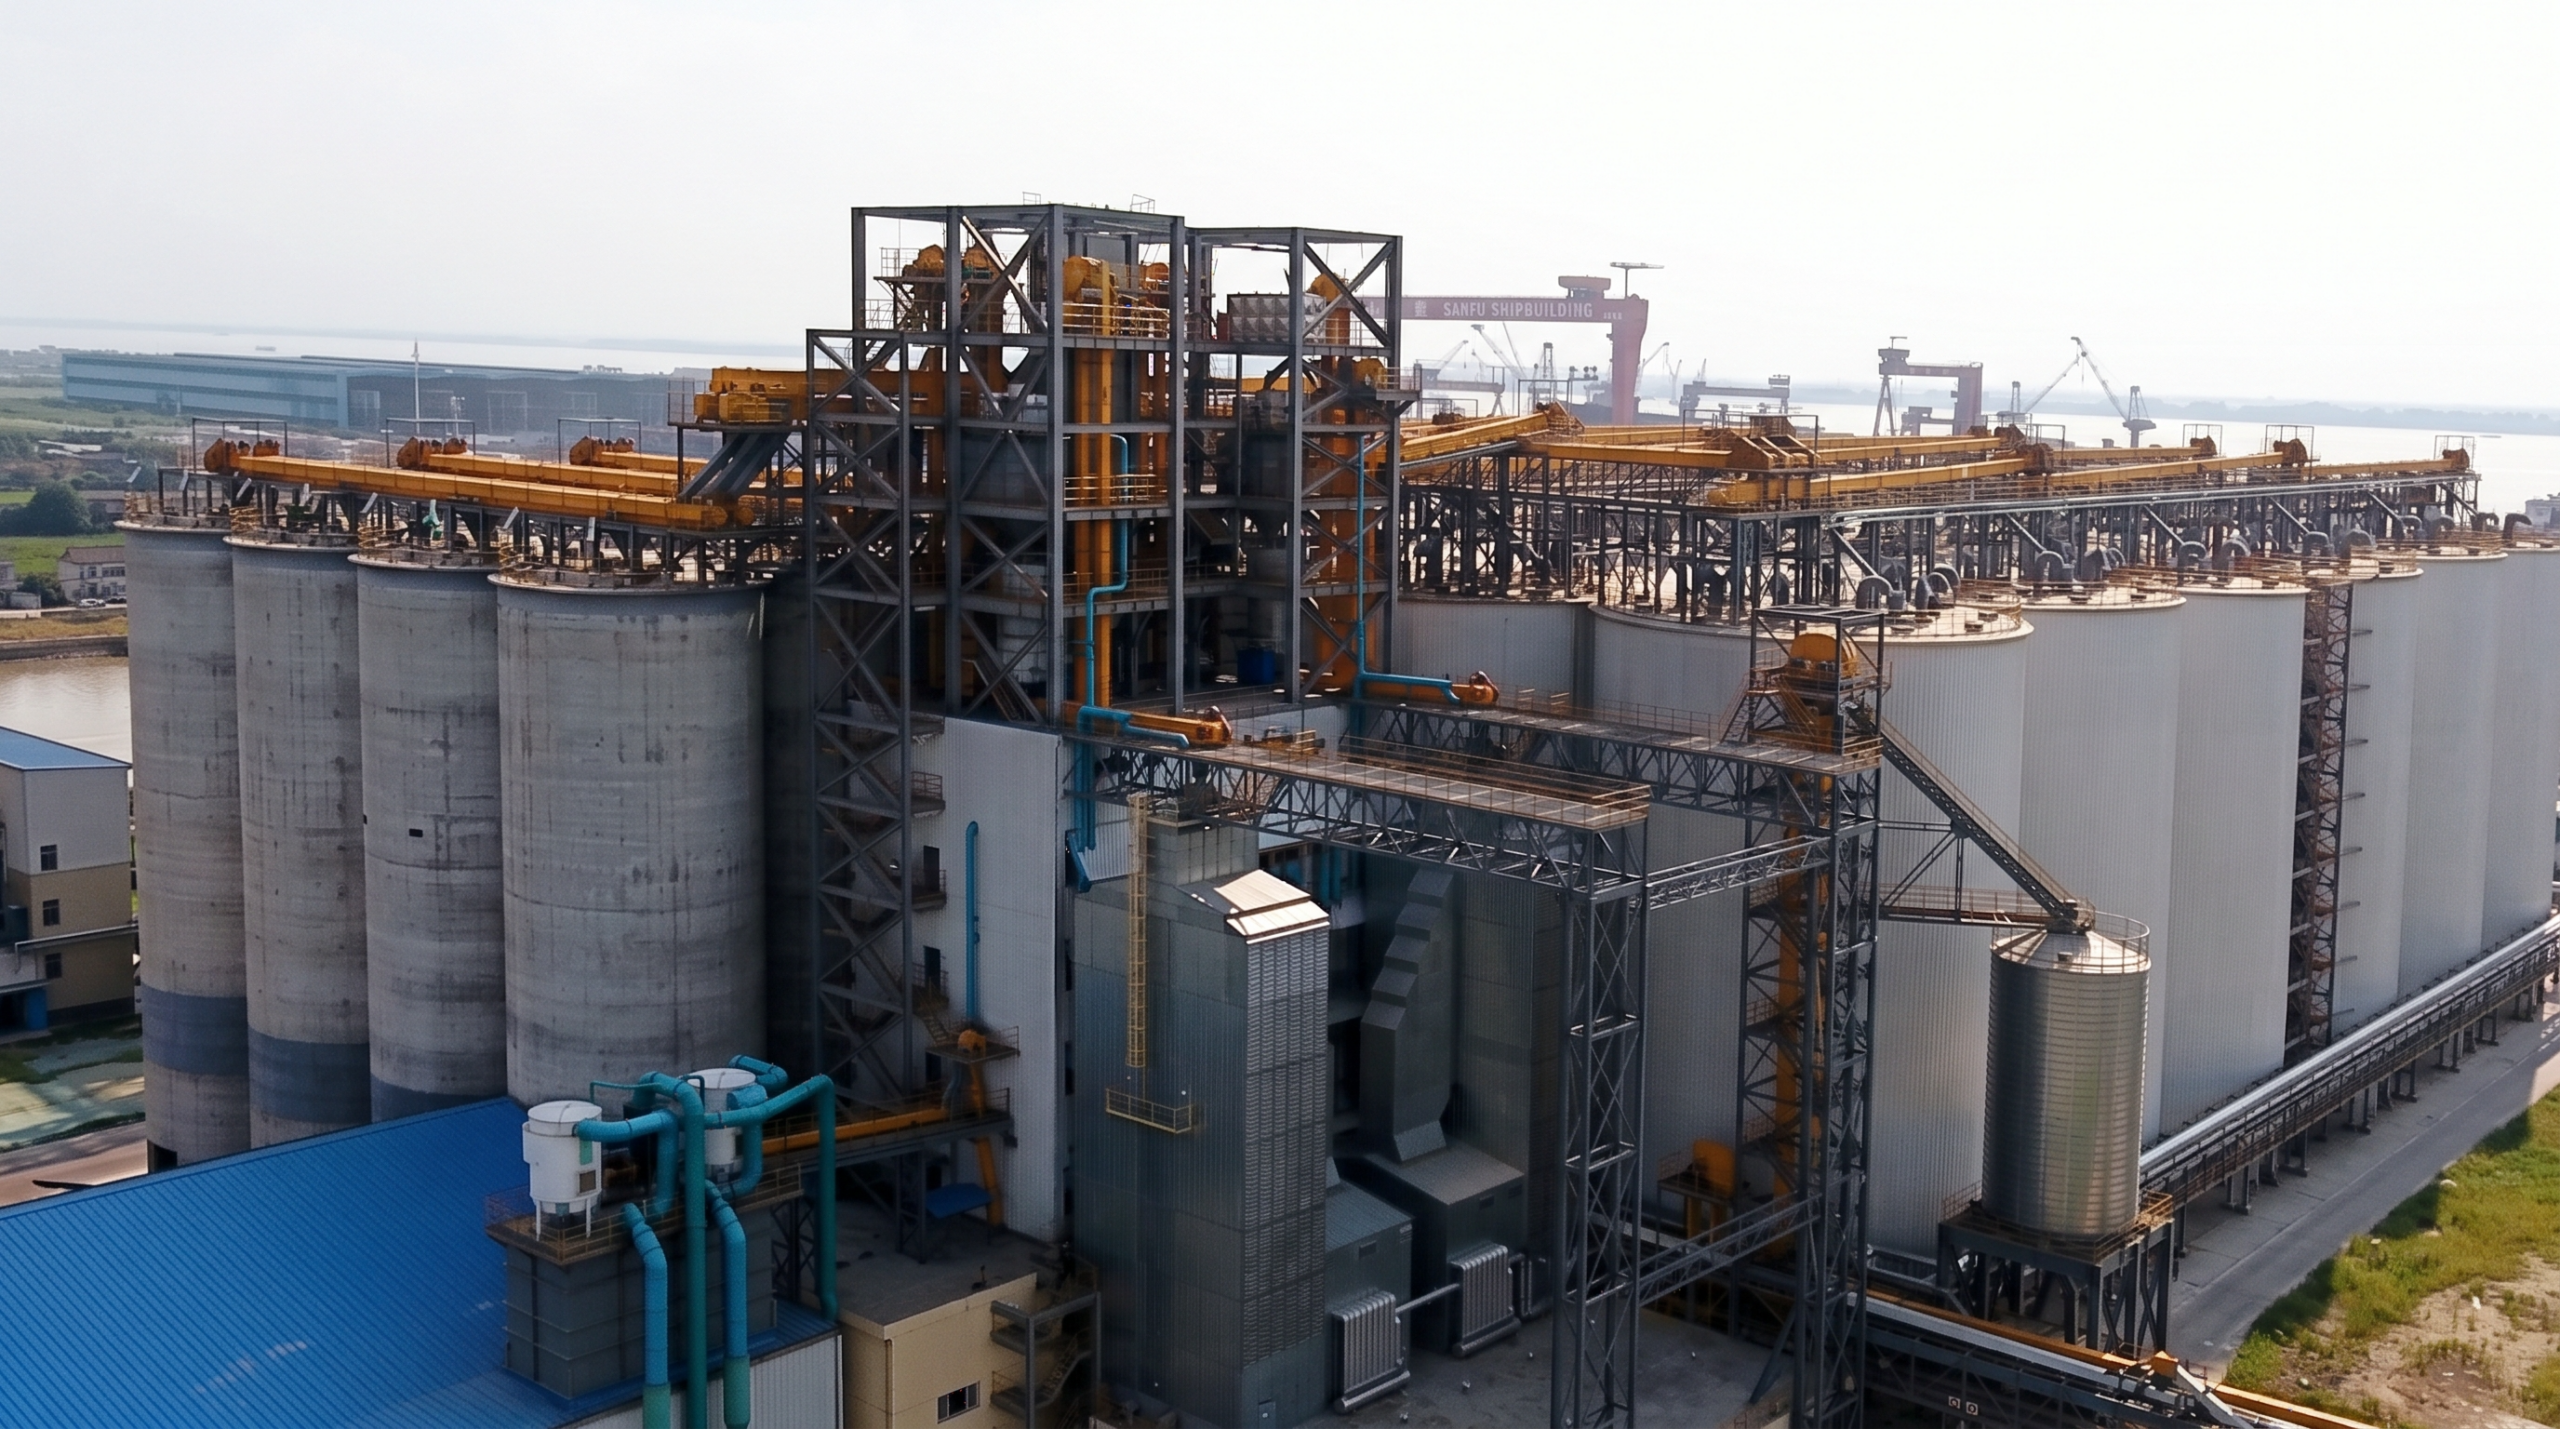
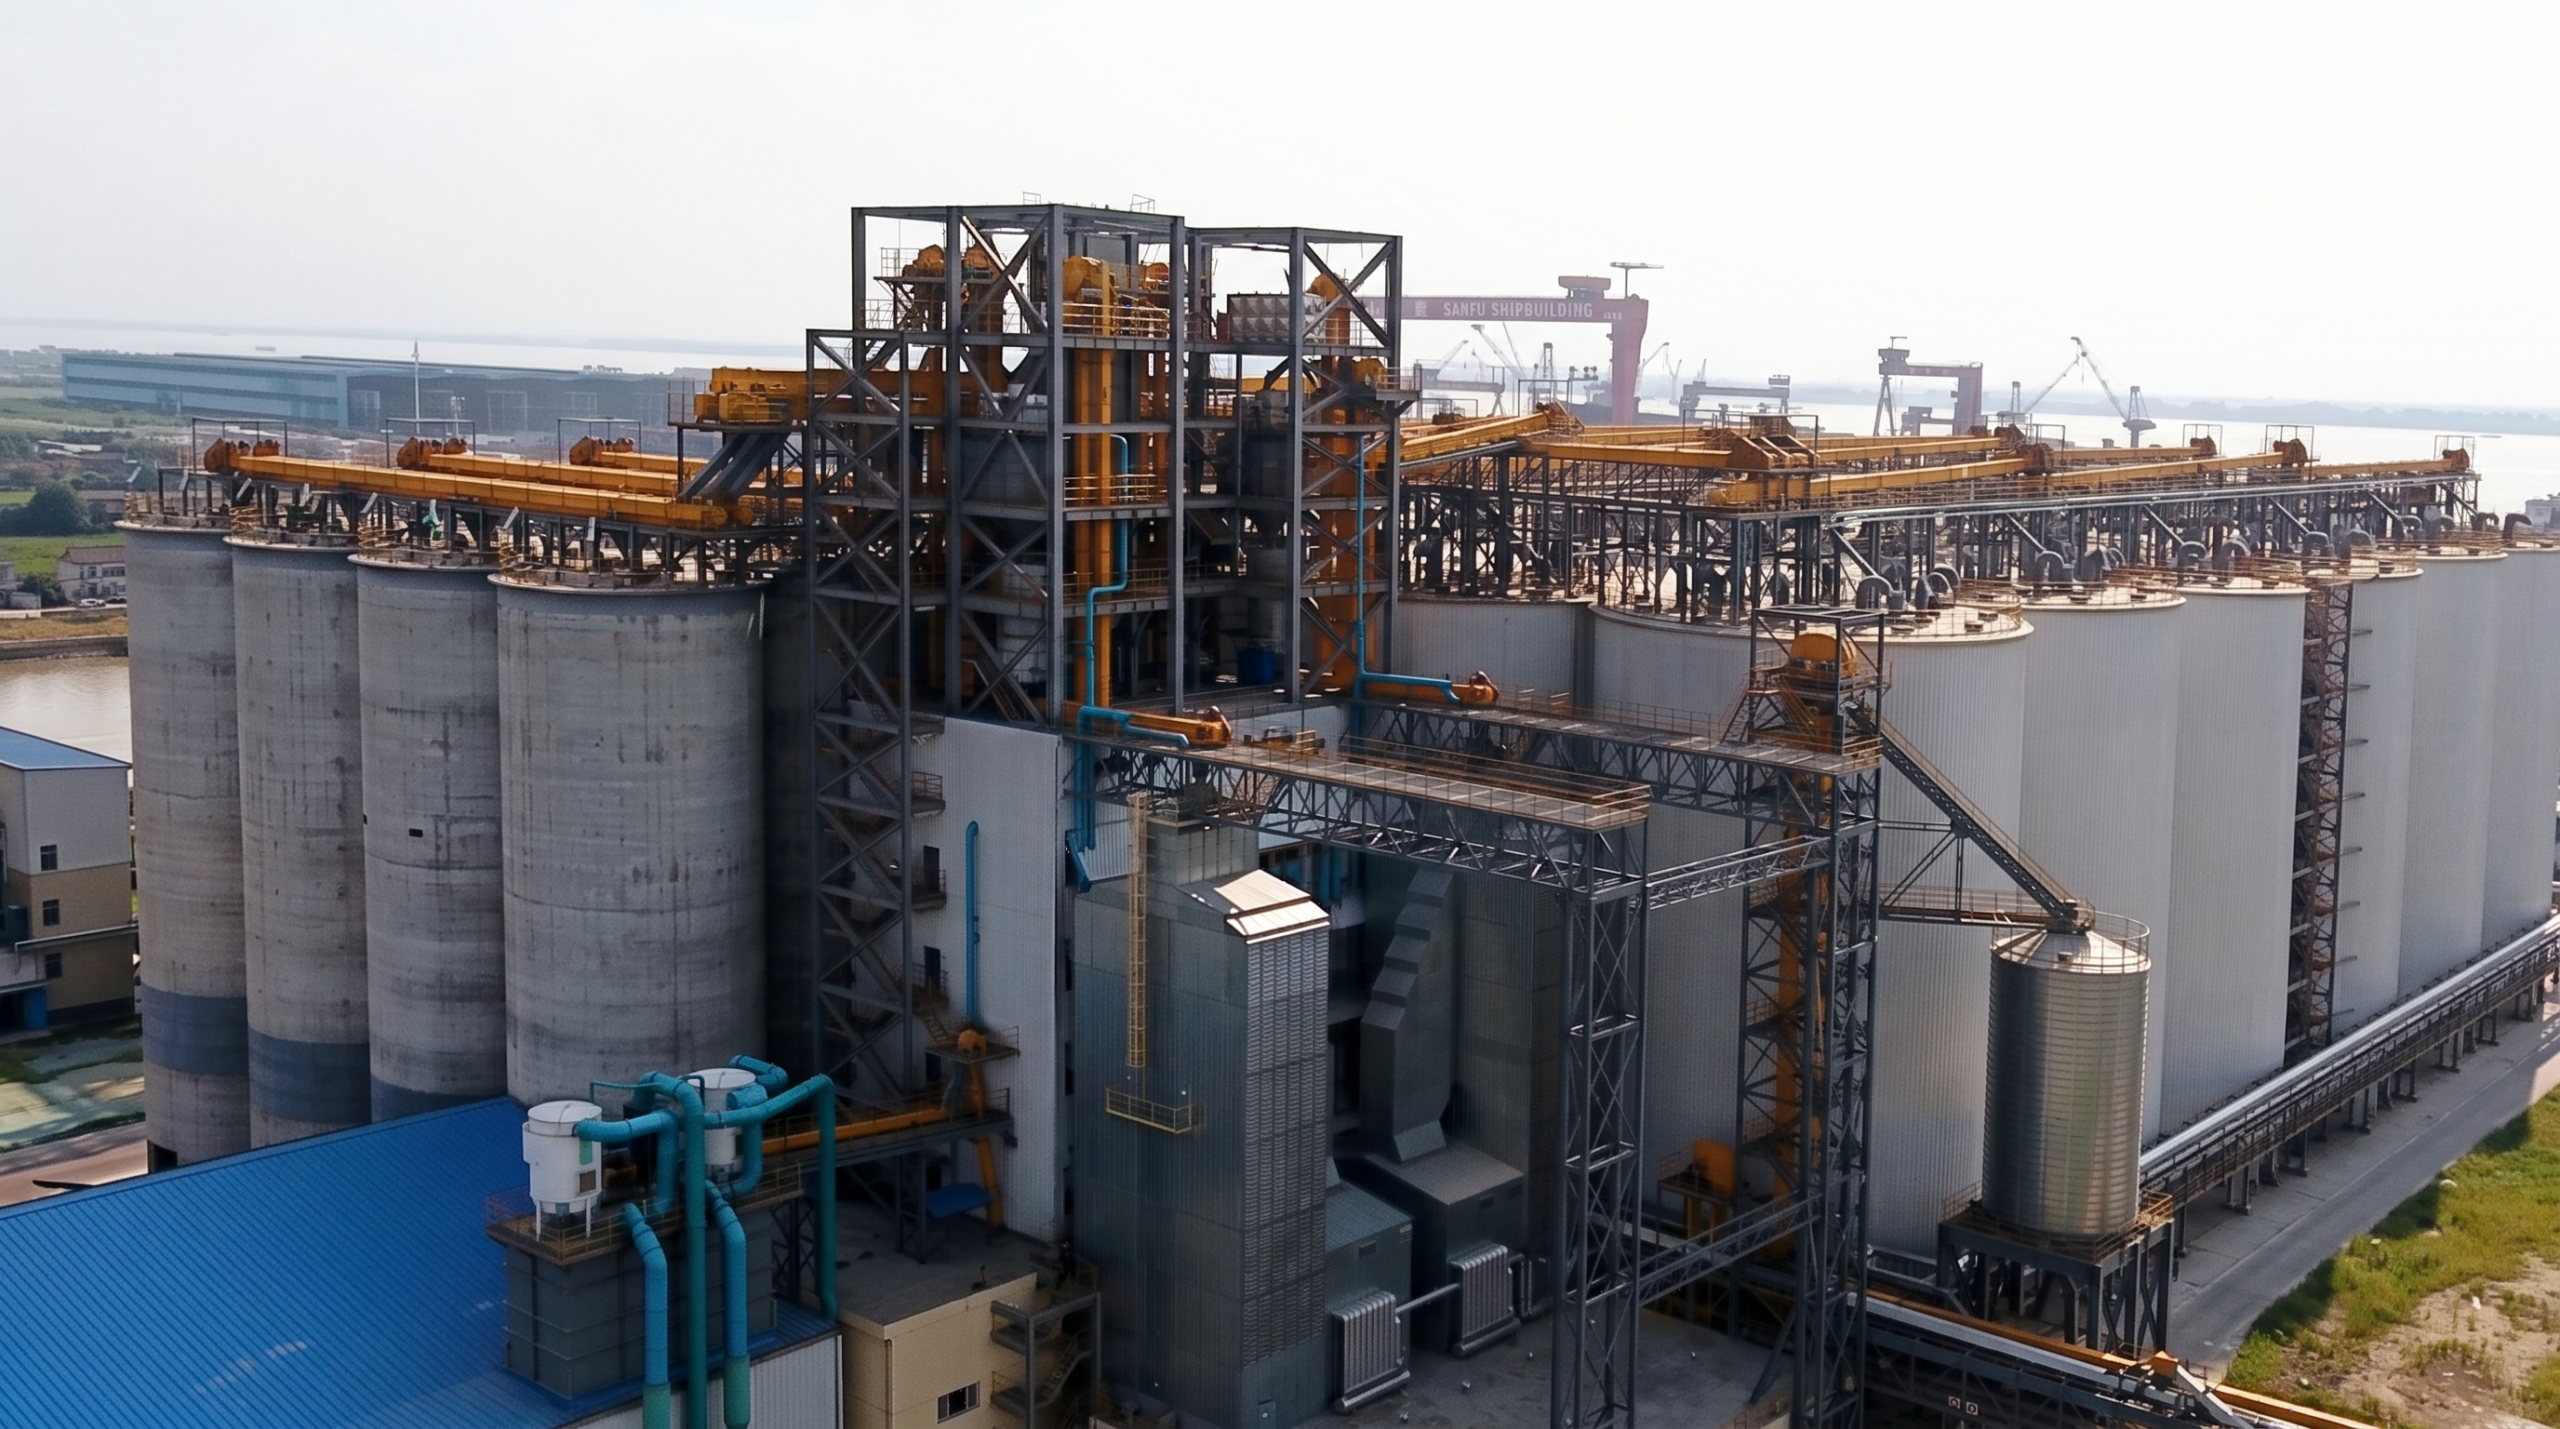
Yihai Kerry (Wilmar Group), operating a flagship smart rice processing base in East China with a daily output of 2,600 tons and an annual capacity of 700,000 tons, required a heavy-duty, high-capacity bulk material handling and continuous grain drying system.
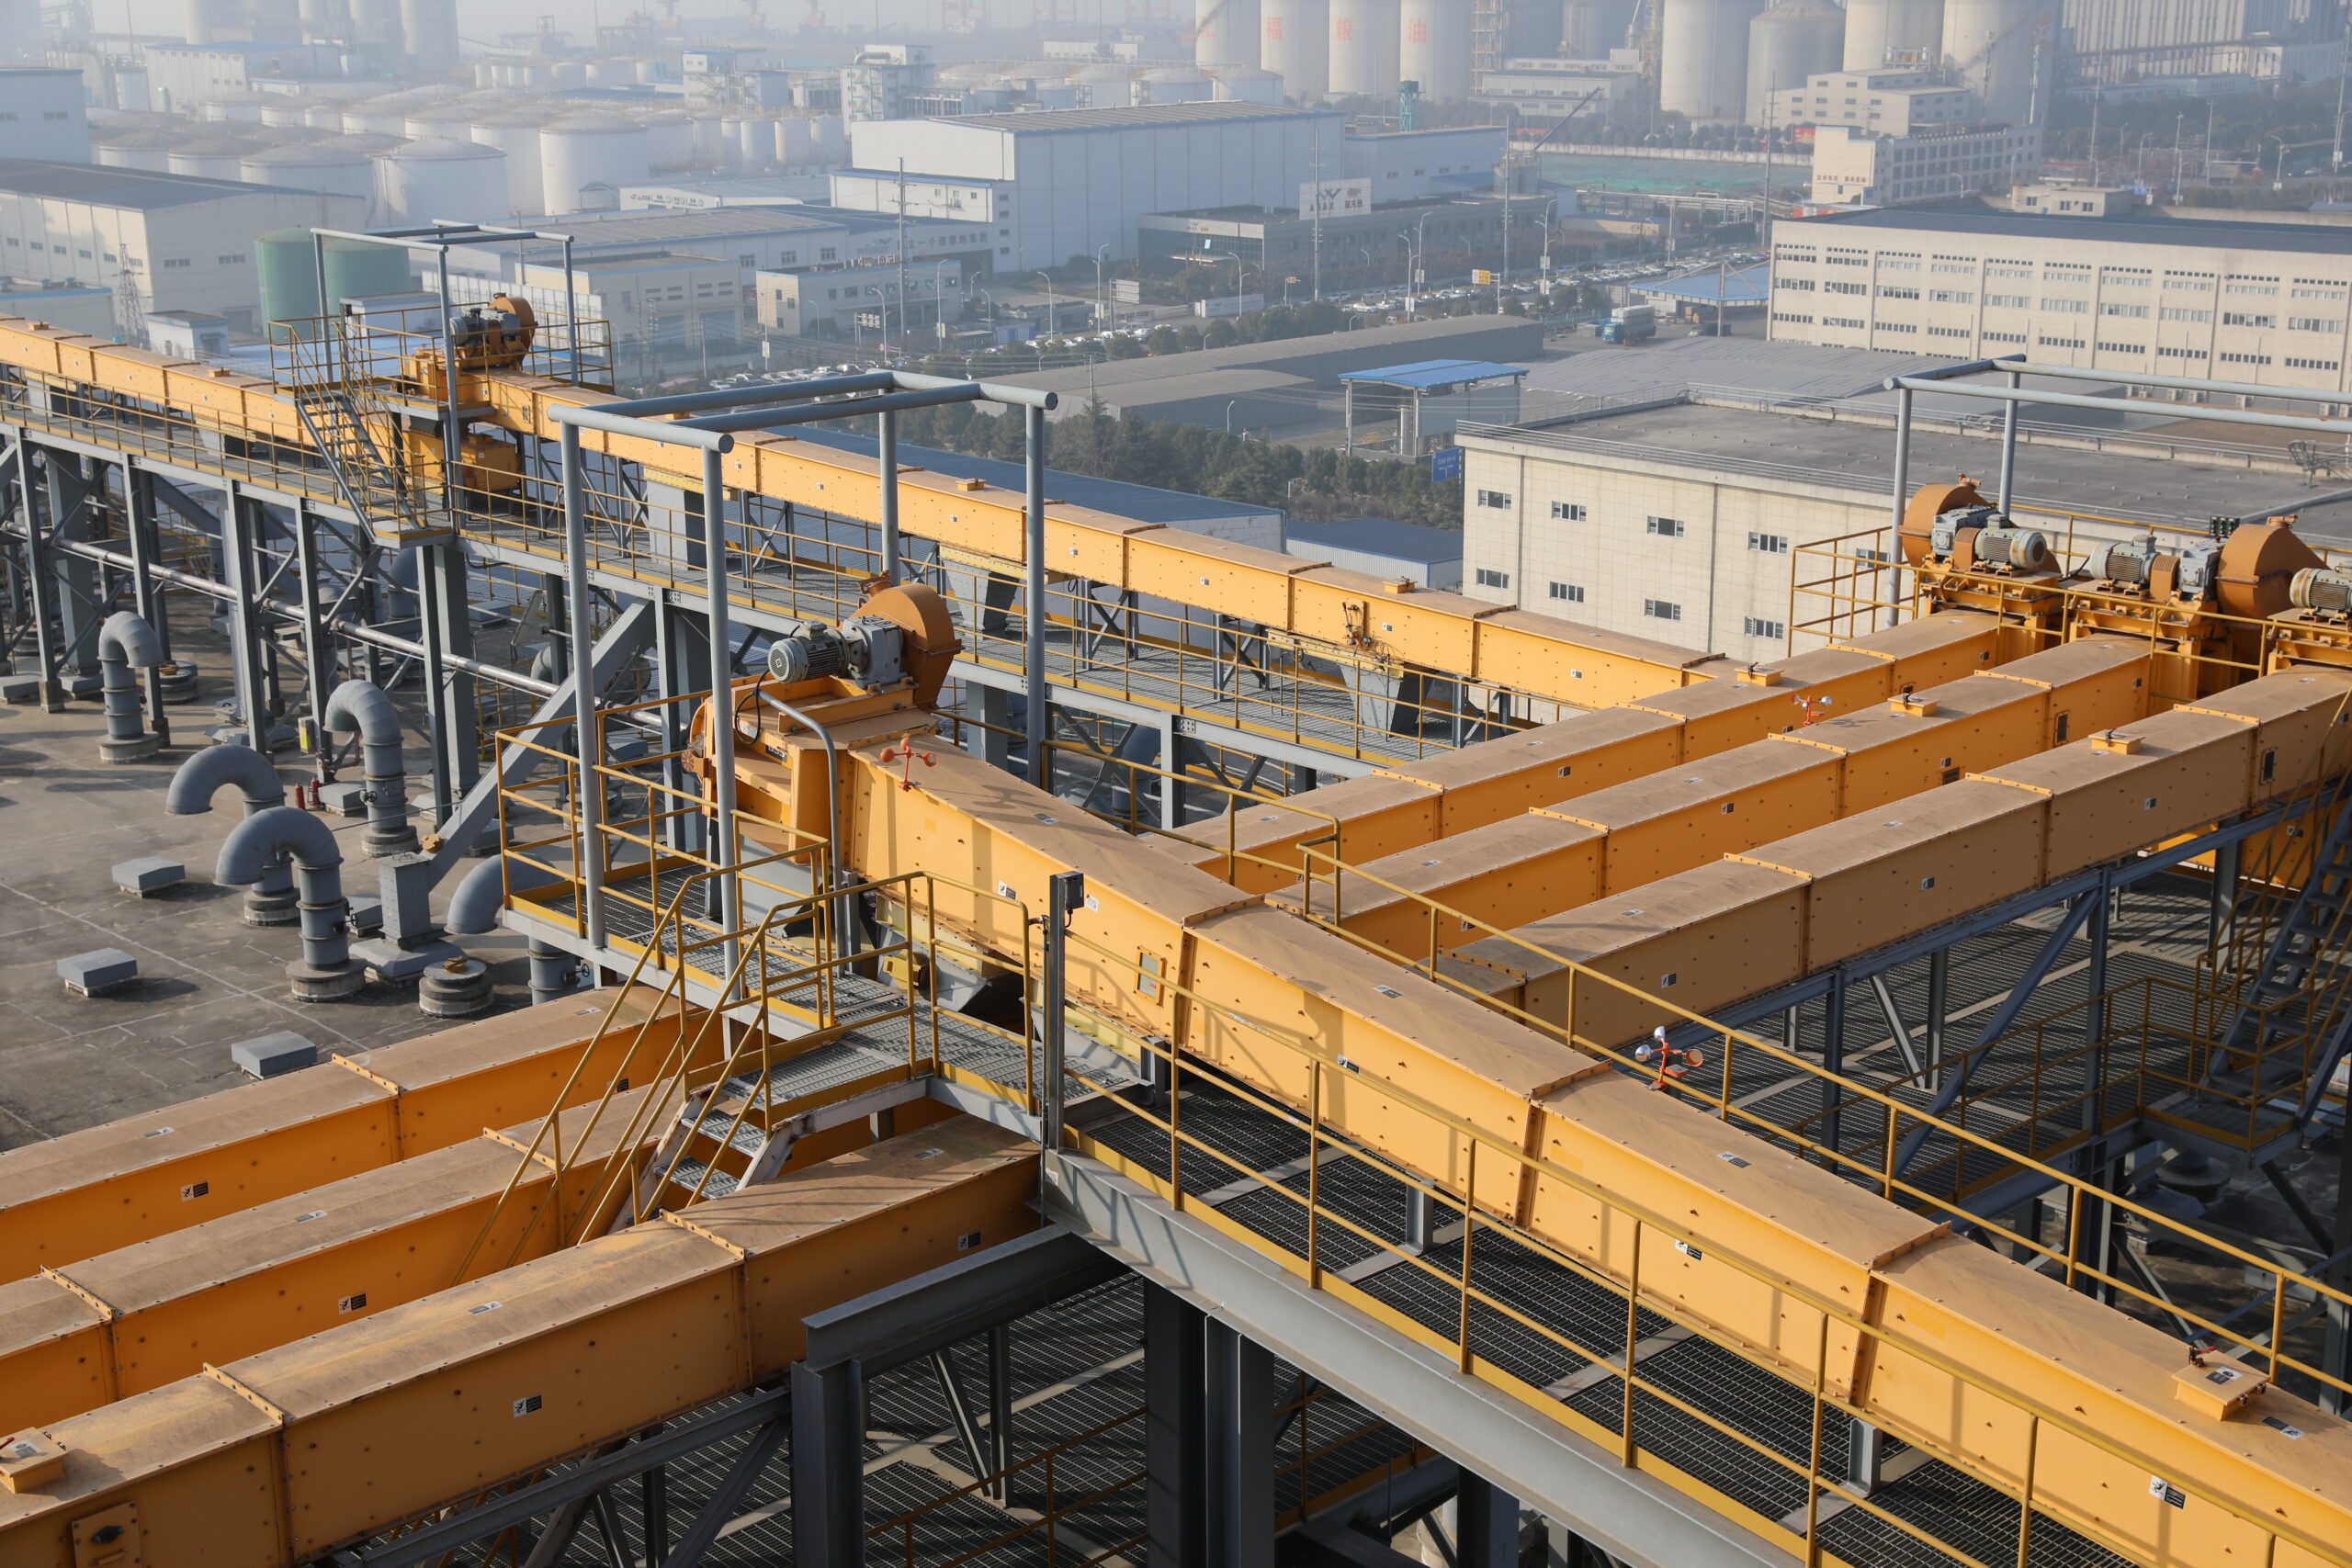
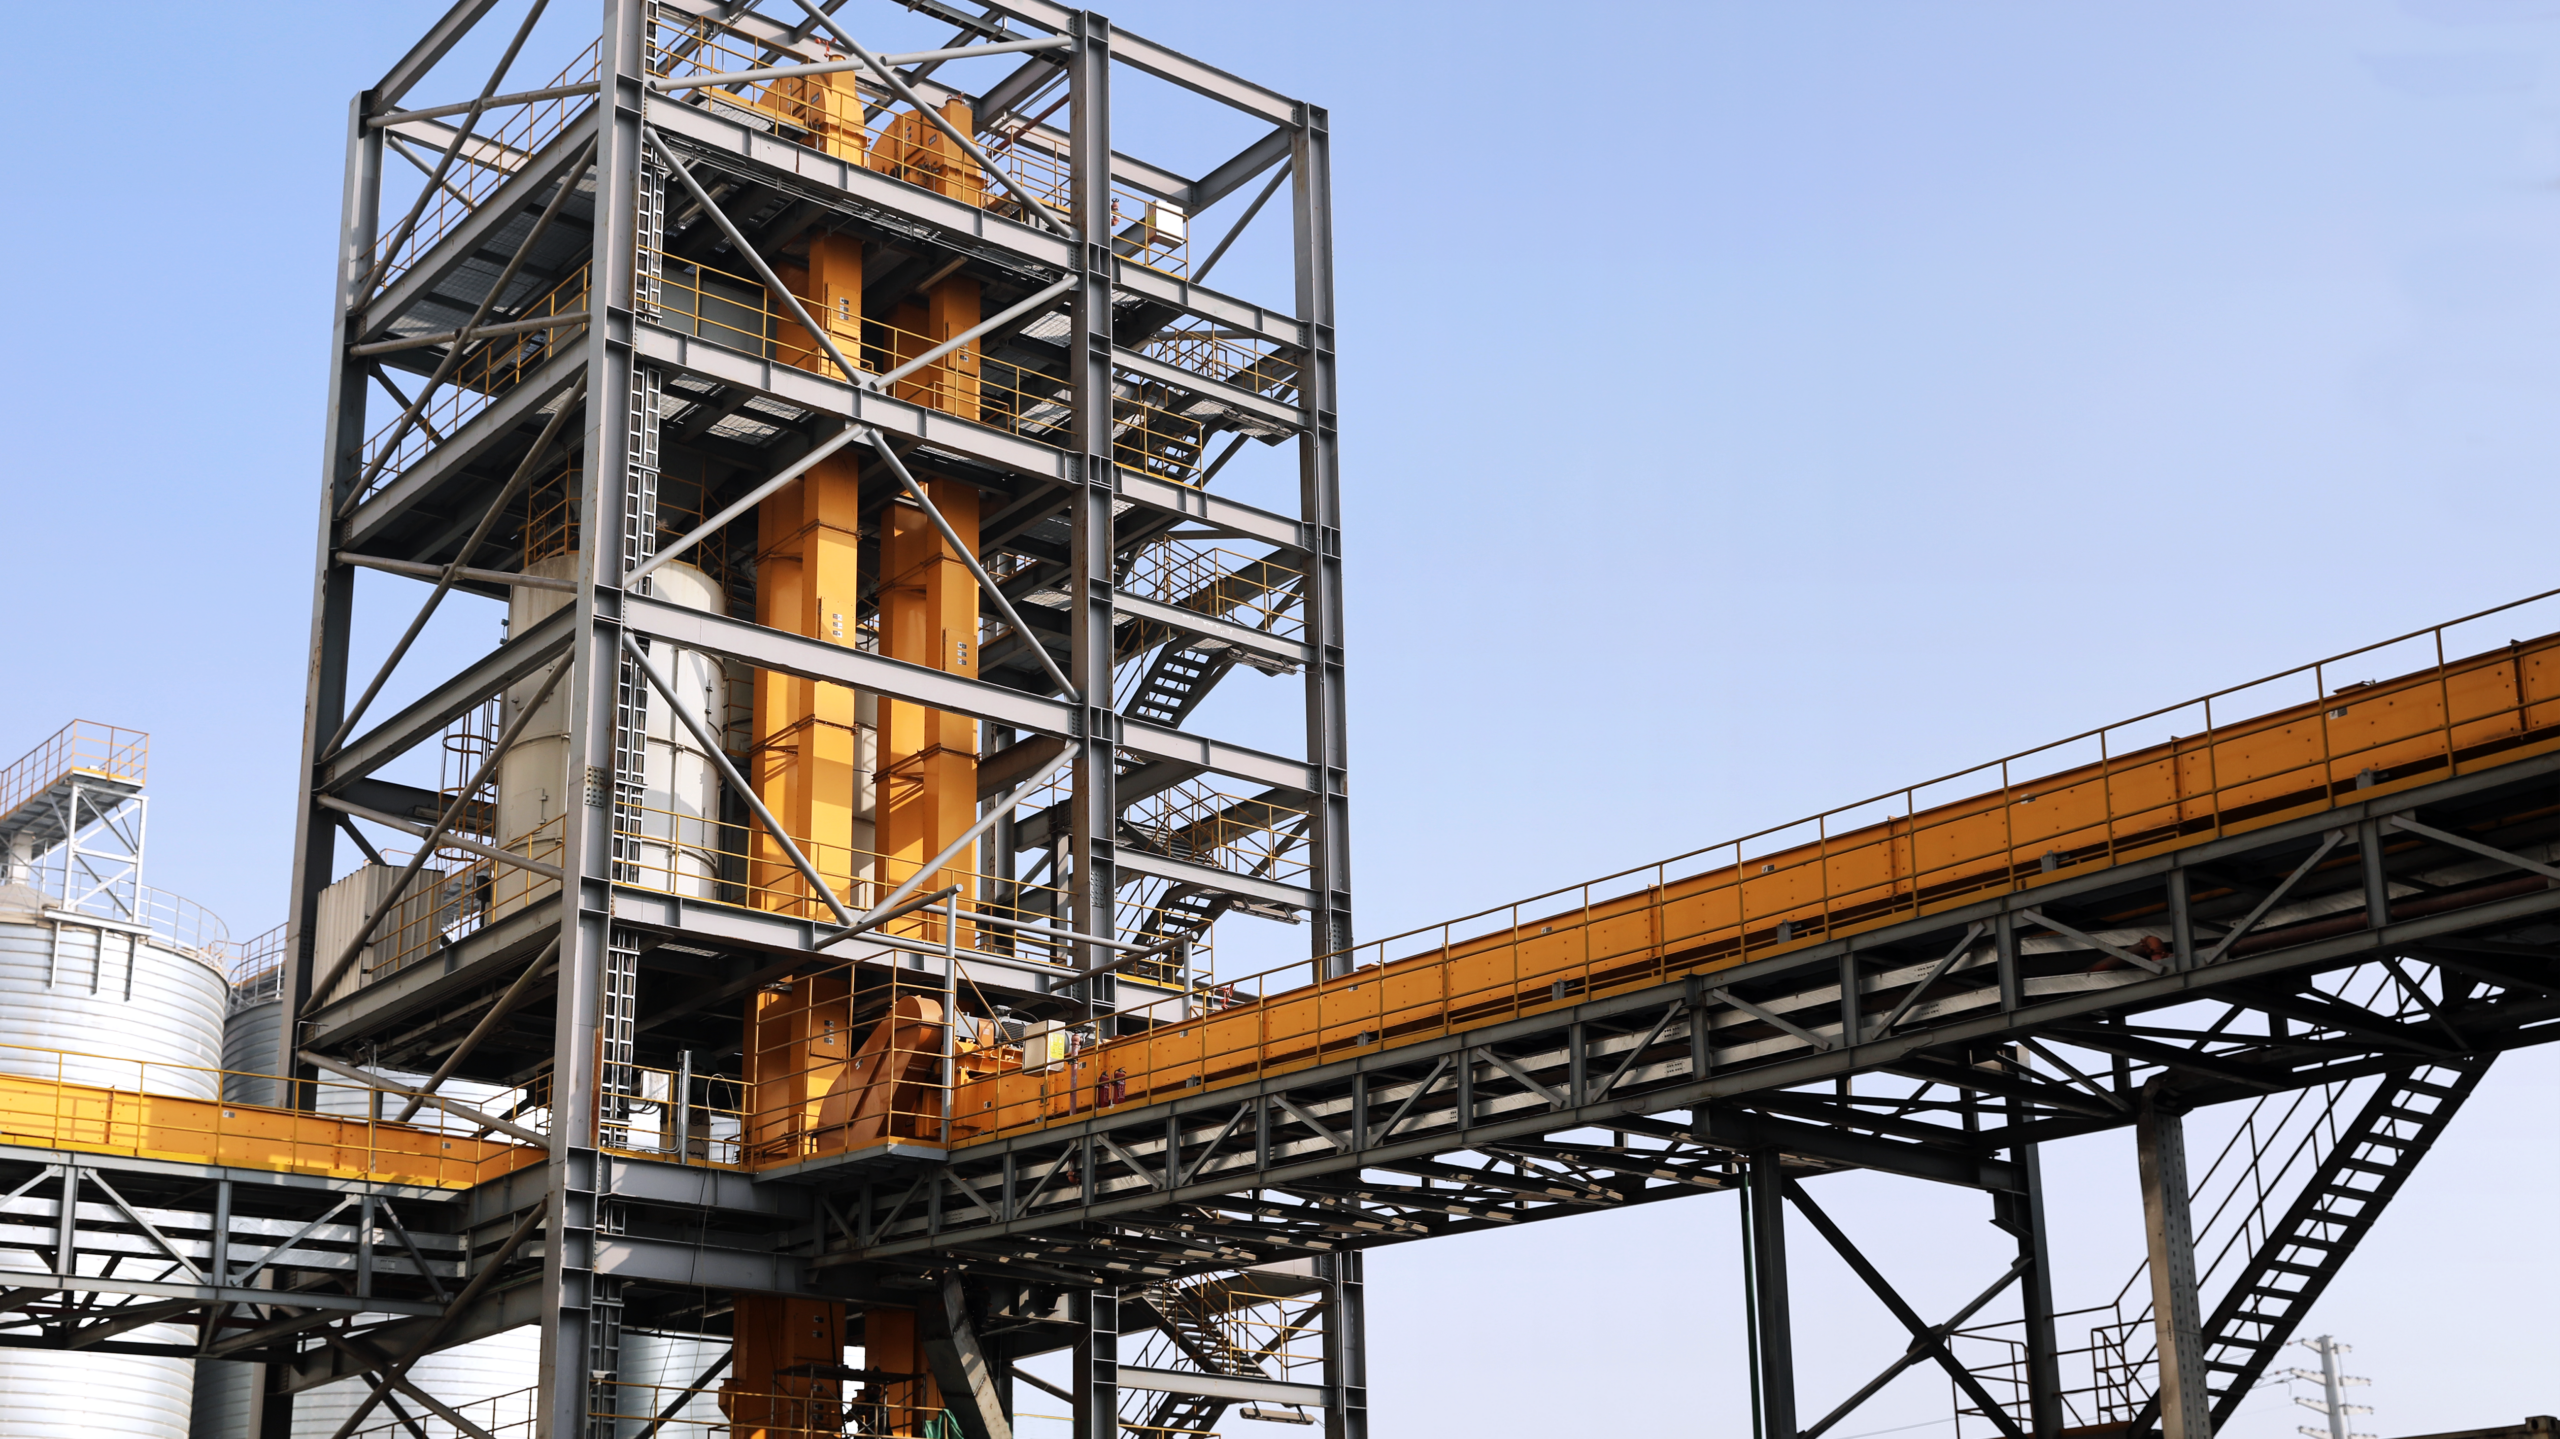
GSS delivered a full set of high-capacity grain drying and conveying equipment for Yihai Kerry’s large-scale rice processing base. The solution covers 1 intelligent continuous grain dryer, 21 multi-capacity paddy bucket elevators, 74 en-masse conveyors for grain and impurity transportation, dedicated impurity drag conveyor and long-distance belt conveyors, supporting stable and high-efficiency continuous rice production.
High-capacity conveying smoothly sustained 24/7 continuous heavy-duty processing; smart drying control protected paddy quality and minimized broken rice; dust-tight enclosure met national green factory standards.
Client Profile: A Mega-Scale Smart Rice Base in East China
Located in the Yangtze River Delta, the Yihai Kerry (Wilmar Group) East China Rice Processing Base is a premier mega-scale smart rice center. Recognized as a national green factory and provincial smart facility, the complex boasts a top-tier daily rice output of 2,600 t/d and an annual processing capacity of 700,000 t/a, serving as a critical strategic hub for regional grain reserves.
Goals & Challenges: 2,600 t/d Daily Output & Precise Low-Breakage Drying
As a mega-scale rice processing hub, the facility faced several universal industry challenges during continuous paddy intake, drying, and transfer:
- 2,600 t/d Ultra-High Daily Output & 24/7 Continuous Operation : Processing 2,600 tons of rice daily demanded high-capacity conveying mainlines capable of sustaining continuous, heavy-duty operation without equipment failure or transfer bottlenecks.
- Precise Moisture Control & Low Rice Breakage : Paddy drying requires strict temperature, humidity, and tempering control to avoid thermal stress. Meanwhile, conveying systems must minimize grain impact to protect head rice yield.
- Dust Control & Green Factory Standards : High-volume paddy intake and screening generate substantial airborne dust. Fully enclosed conveying and automated controls are mandatory to satisfy national green factory standards.
Customized Solution: High-Capacity Conveying & Smart Drying Package
To meet Wilmar’s heavy-duty operational and quality standards, GSS delivered a customized, high-capacity bulk material handling and drying package specifically engineered for processing paddy:
- Continuous Grain Drying & Control Package : Installed 1 unit of high-capacity continuous grain dryer paired with an intelligent electric control architecture to manage large-scale paddy drying, tempering, and cooling for consistent processing quality.
- High-Capacity Paddy Bucket Elevators (21 units) : Deployed 21 units of paddy bucket elevators, including 9 units at 250 t/h , 6 units at 150 t/h , 2 units at 120 t/h , and 4 units at 50 t/h, providing reliable vertical elevation.
- Dust-Tight En-Masse Conveyors (74 units) : Deployed 74 units o en-masse conveyors, including 51 units at 250 t/h , 18 units at 150 t/h, 4 units at 120 t/h, and 1 unit at 10 t/h for impurity handling, delivering dust-free horizontal transport across intake, screening, and milling lines.
- Belt & Up-Load Drag Conveyor Package (3 units) : Deployed 2 units of 250 t/h belt conveyors for long-distance paddy transfer, and 1 unit of 10 t/h up-load drag conveyor for flexible impurity discharge.
Project Value: Mega Capacity, Quality Protection, and Green Smart Standards
Mega-Capacity
GSS high-capacity equipment (up to 250 t/h) effortlessly withstands 24/7 heavy-duty operation, ensuring low-downtime material flow for Wilmar's flagship rice line.
Low-Breakage
Intelligent drying controls paired with low-breakage GSS bucket elevators and en-masse conveyors protect kernel integrity, boosting head rice yield and market competitiveness.
Eco-Friendly
High automation and dust-tight design eliminated dust pollution and lowered maintenance costs, fully aligning with national green factory and smart facility standards.
"Operating a mega-scale smart rice base with a daily output of 2,600 tons demands exceptional equipment stability and strict grain quality control. The complete grain drying and bulk handling system provided by GSS has performed brilliantly under continuous full-load operations. Its 250 t/h conveying lines handle high-volume paddy transfer seamlessly, while the smart dryer and low-breakage conveyors ensure optimal finished rice quality. GSS has provided robust technical support for our green, high-capacity production line."