Long-Distance Dust-Free Grain Conveying System | Yihai Kerry East China Seaport Flour Base
Key Highlights
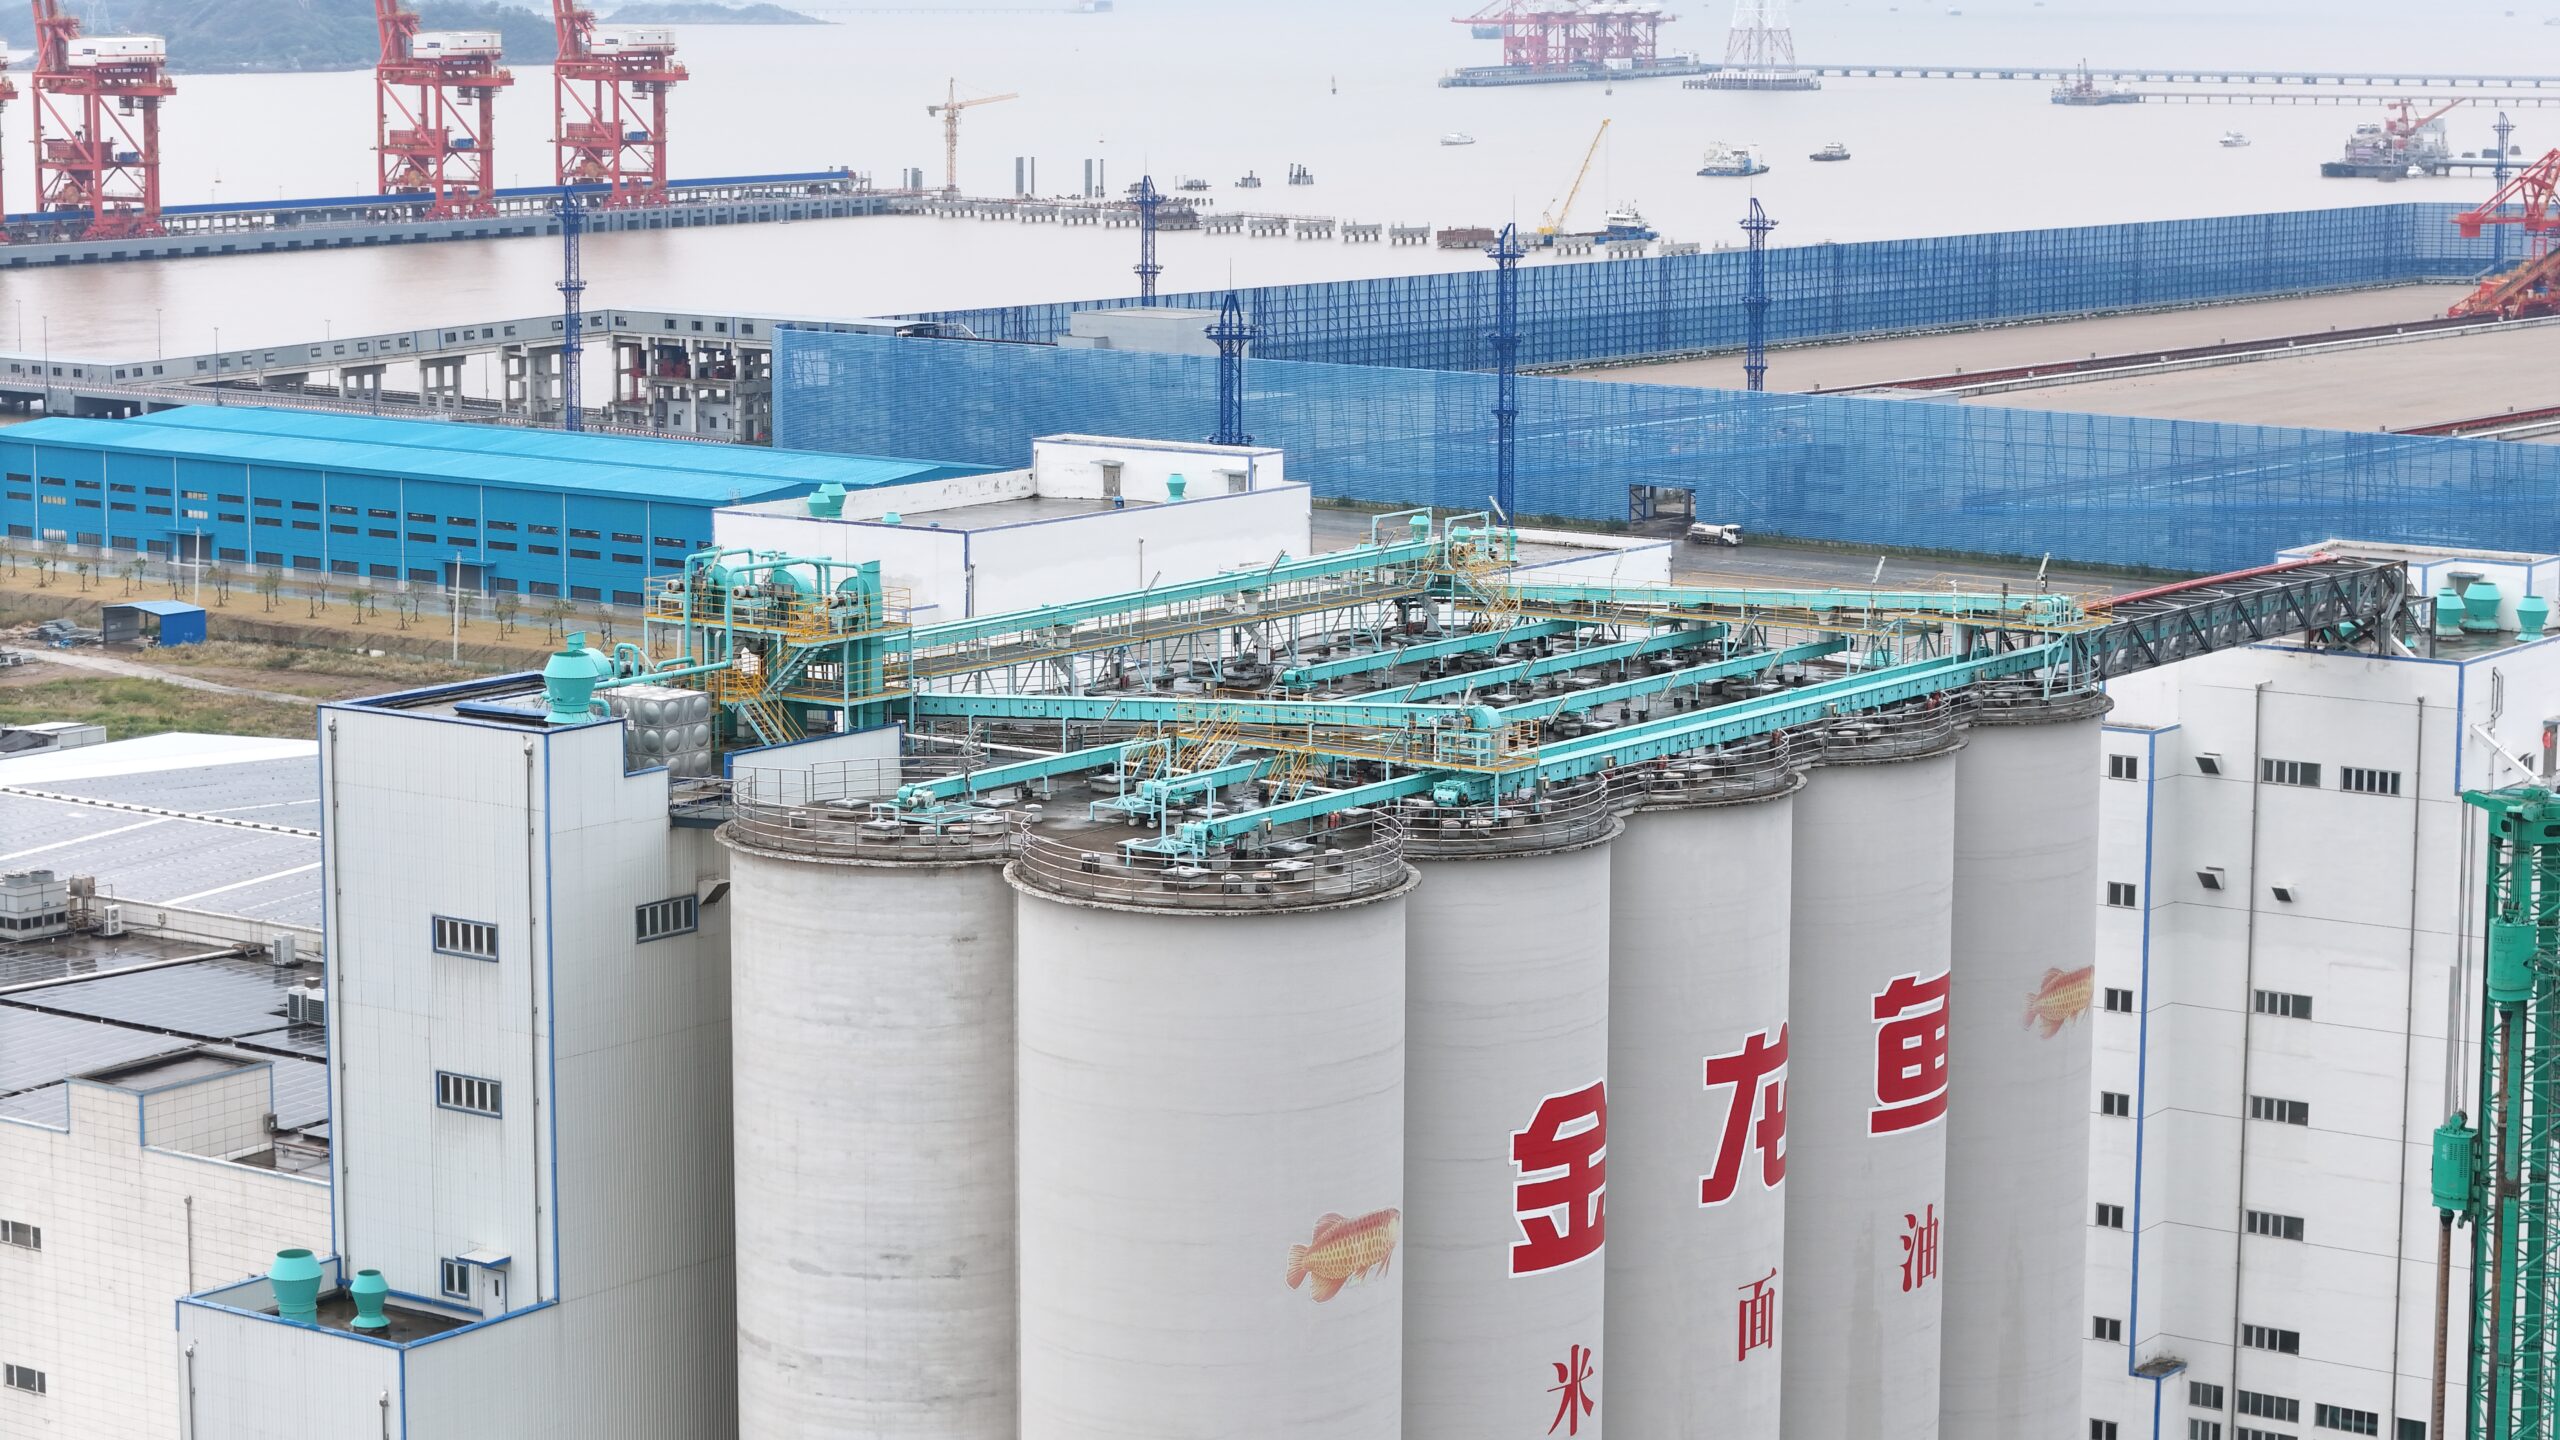
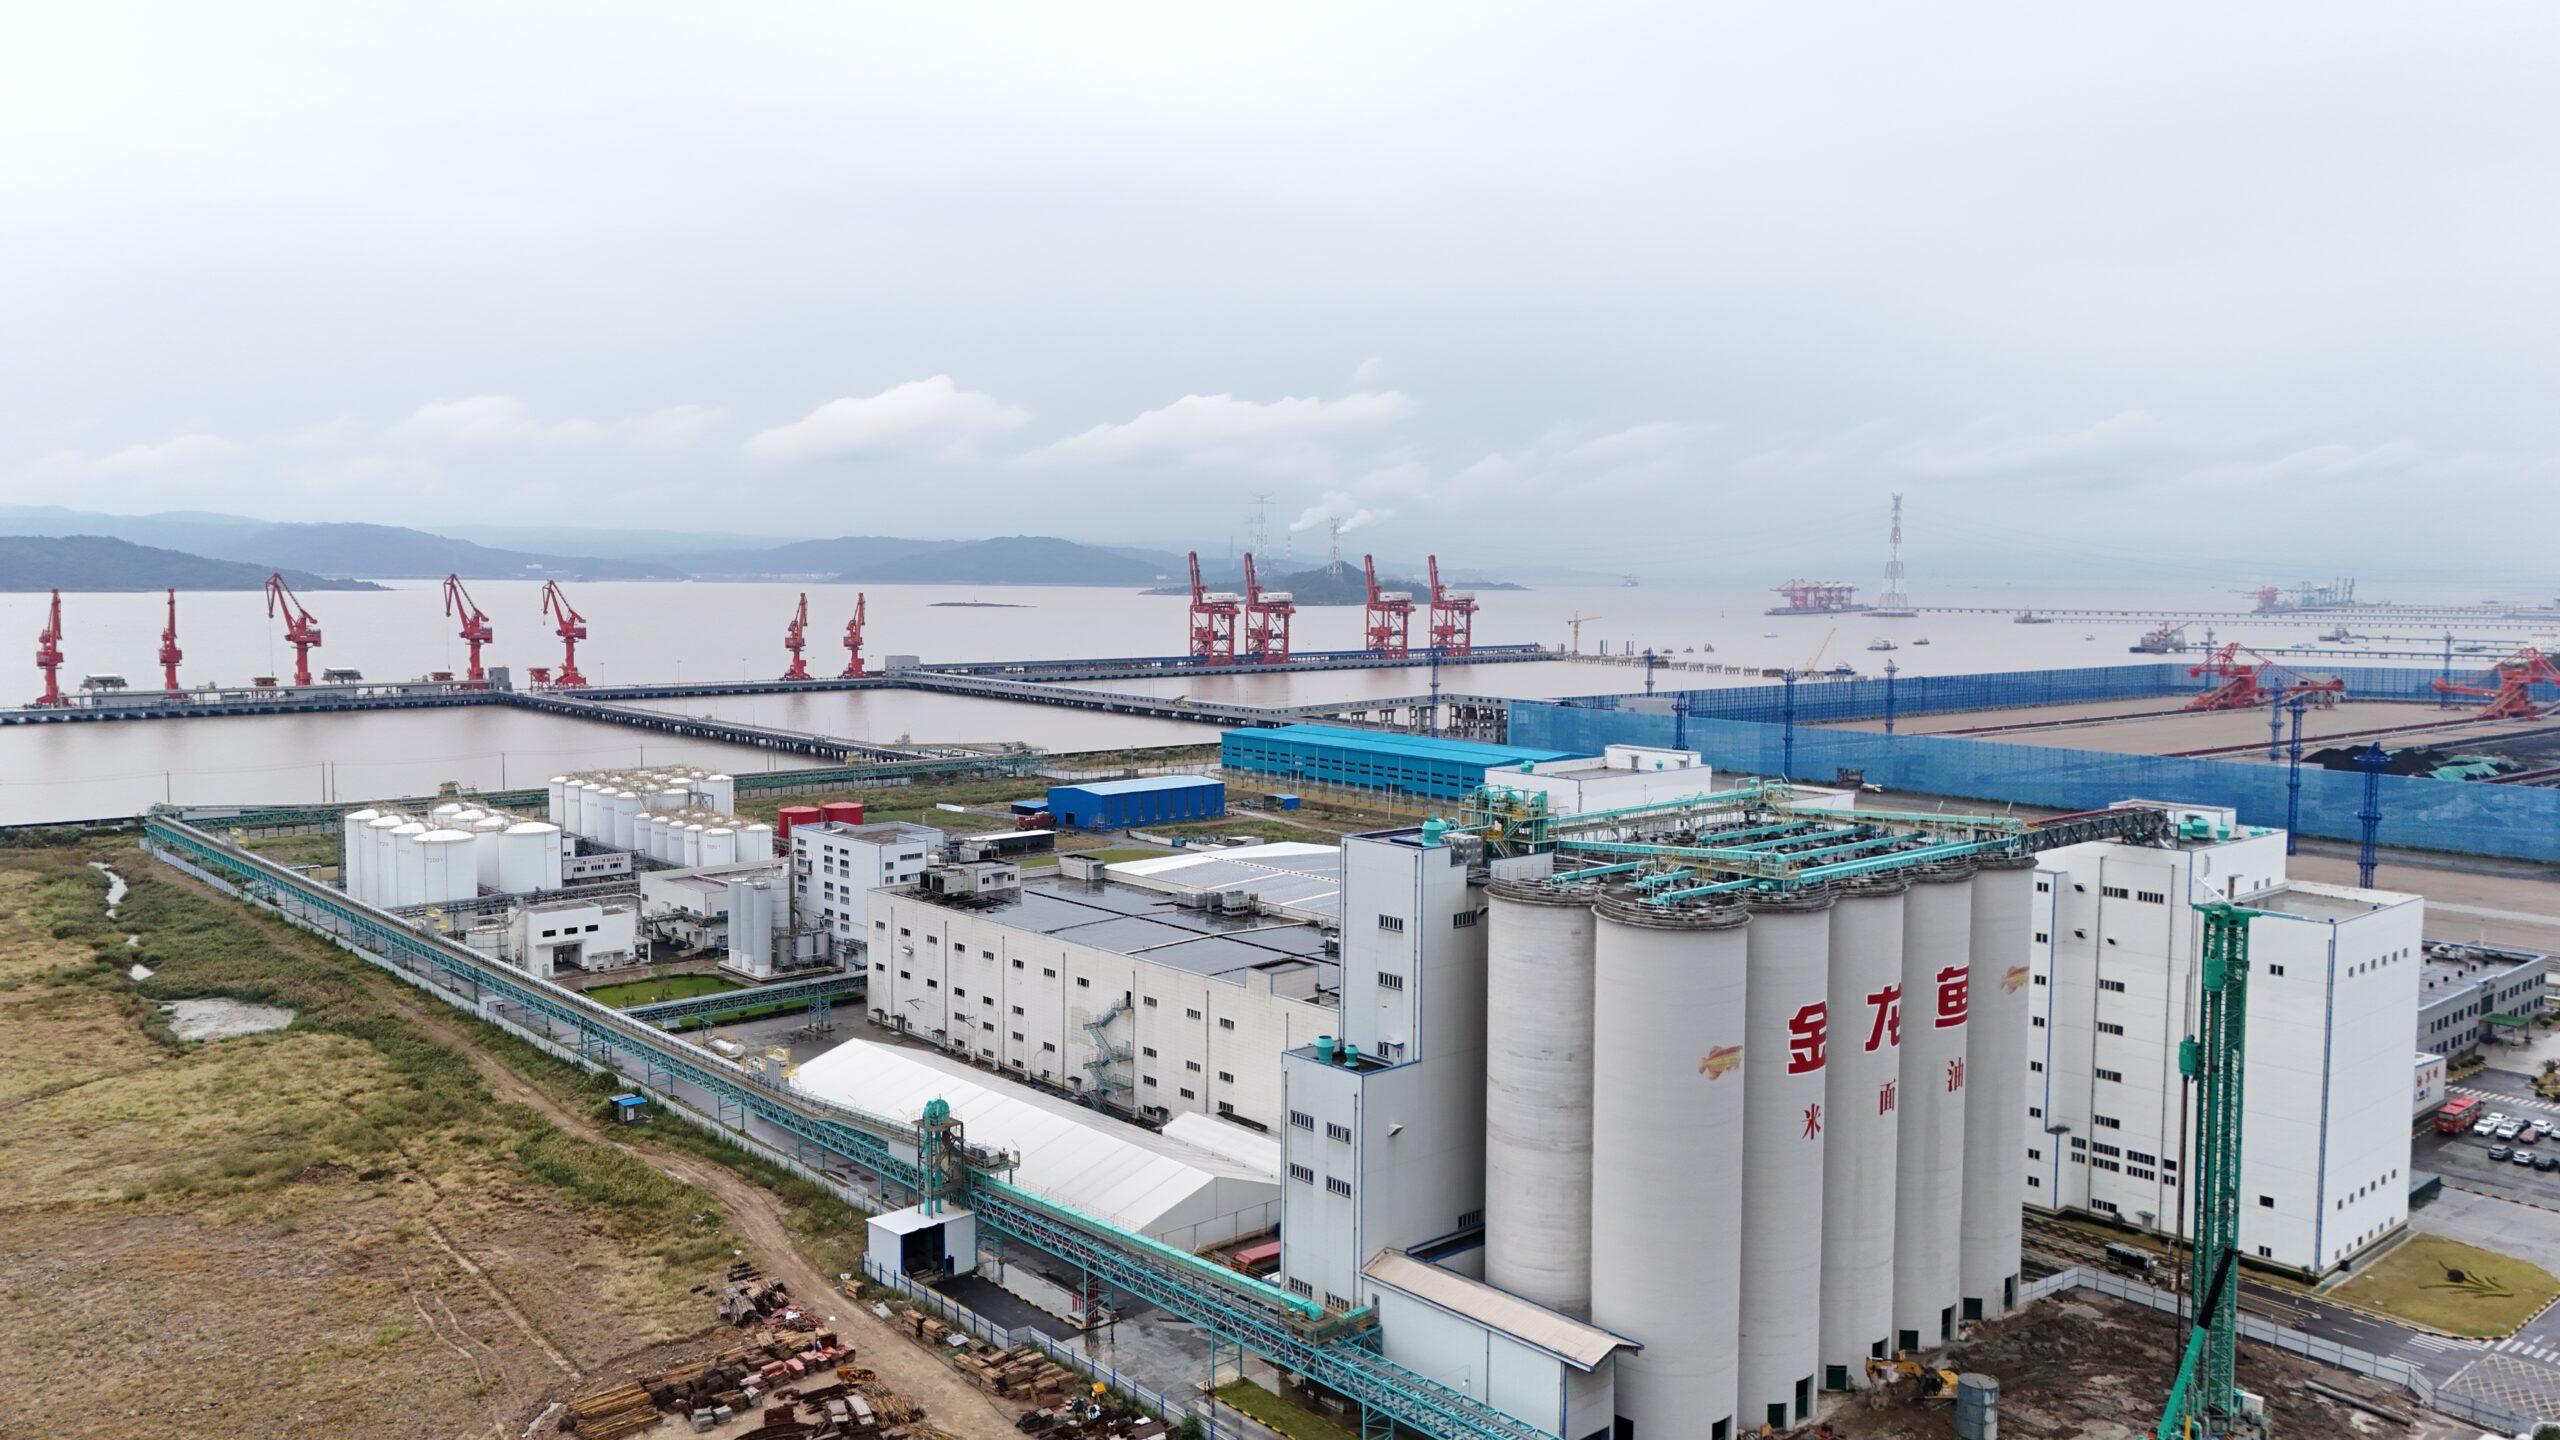
Yihai Kerry (Wilmar Group), operating a major seaport terminal flour processing complex in East China with an annual port throughput of 4.5 million tons, required a long-distance, high-capacity grain conveying system and a dust-free wheat intake system to connect its terminal dock directly to storage silos and milling facilities.
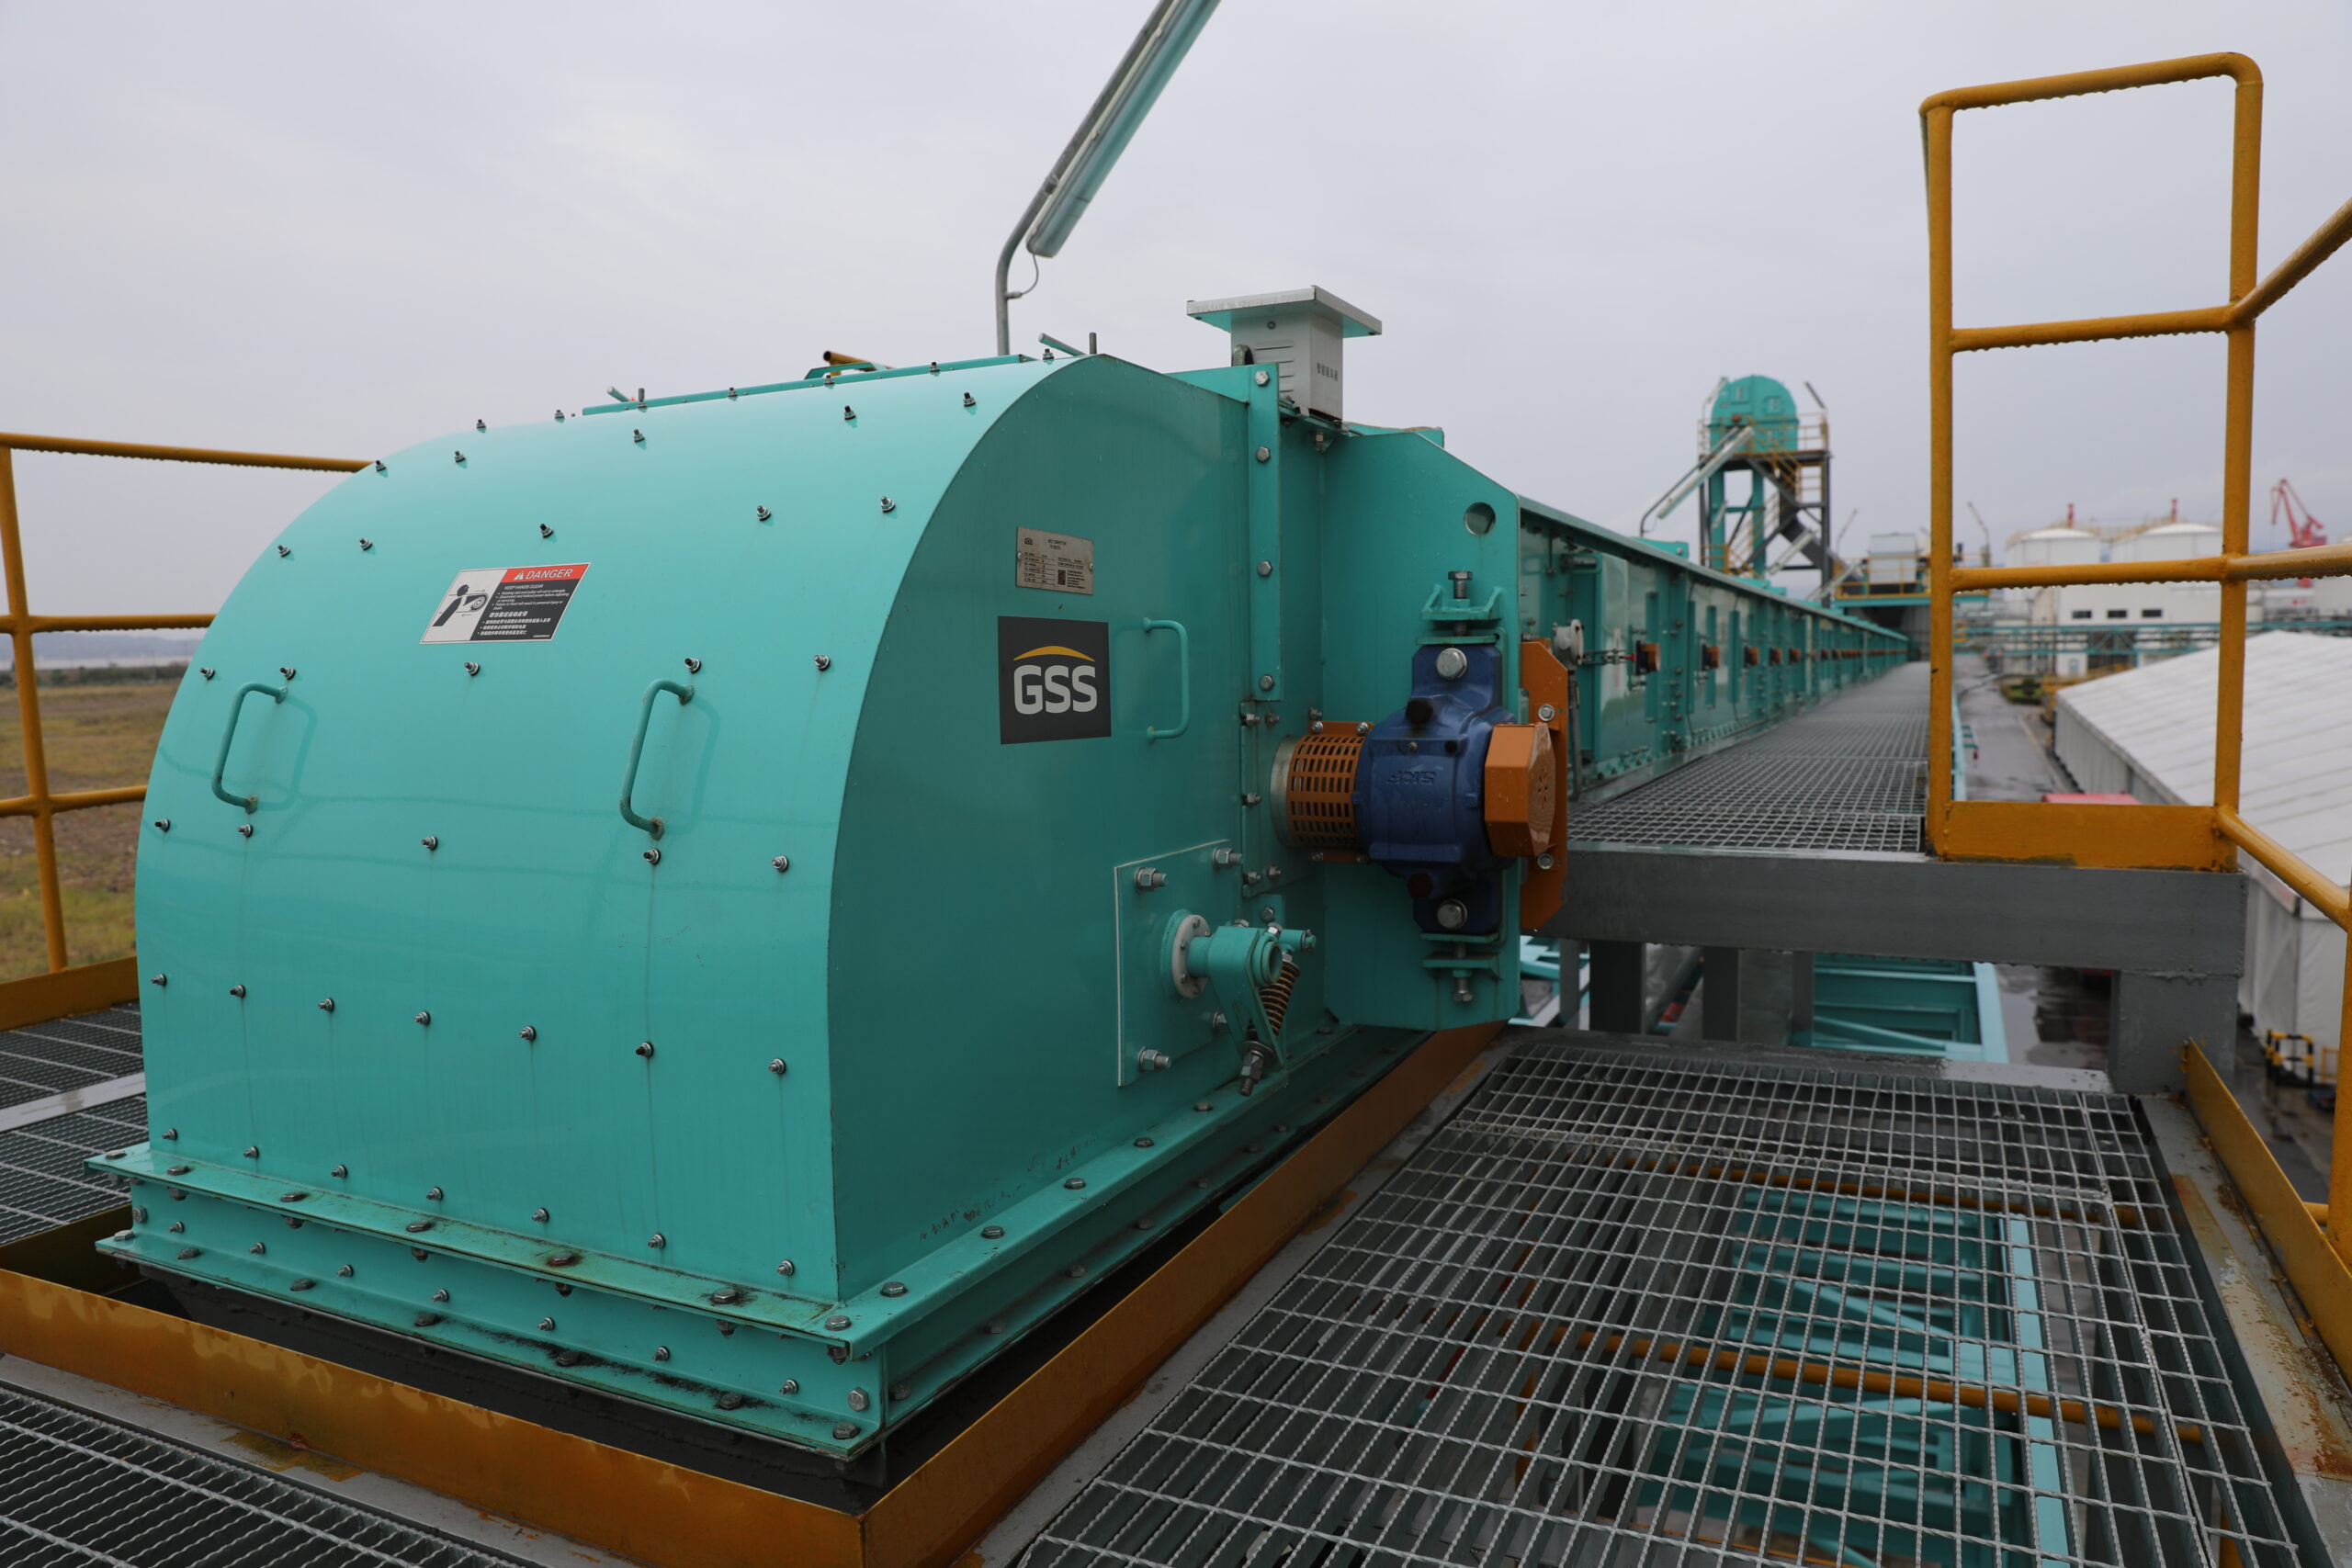
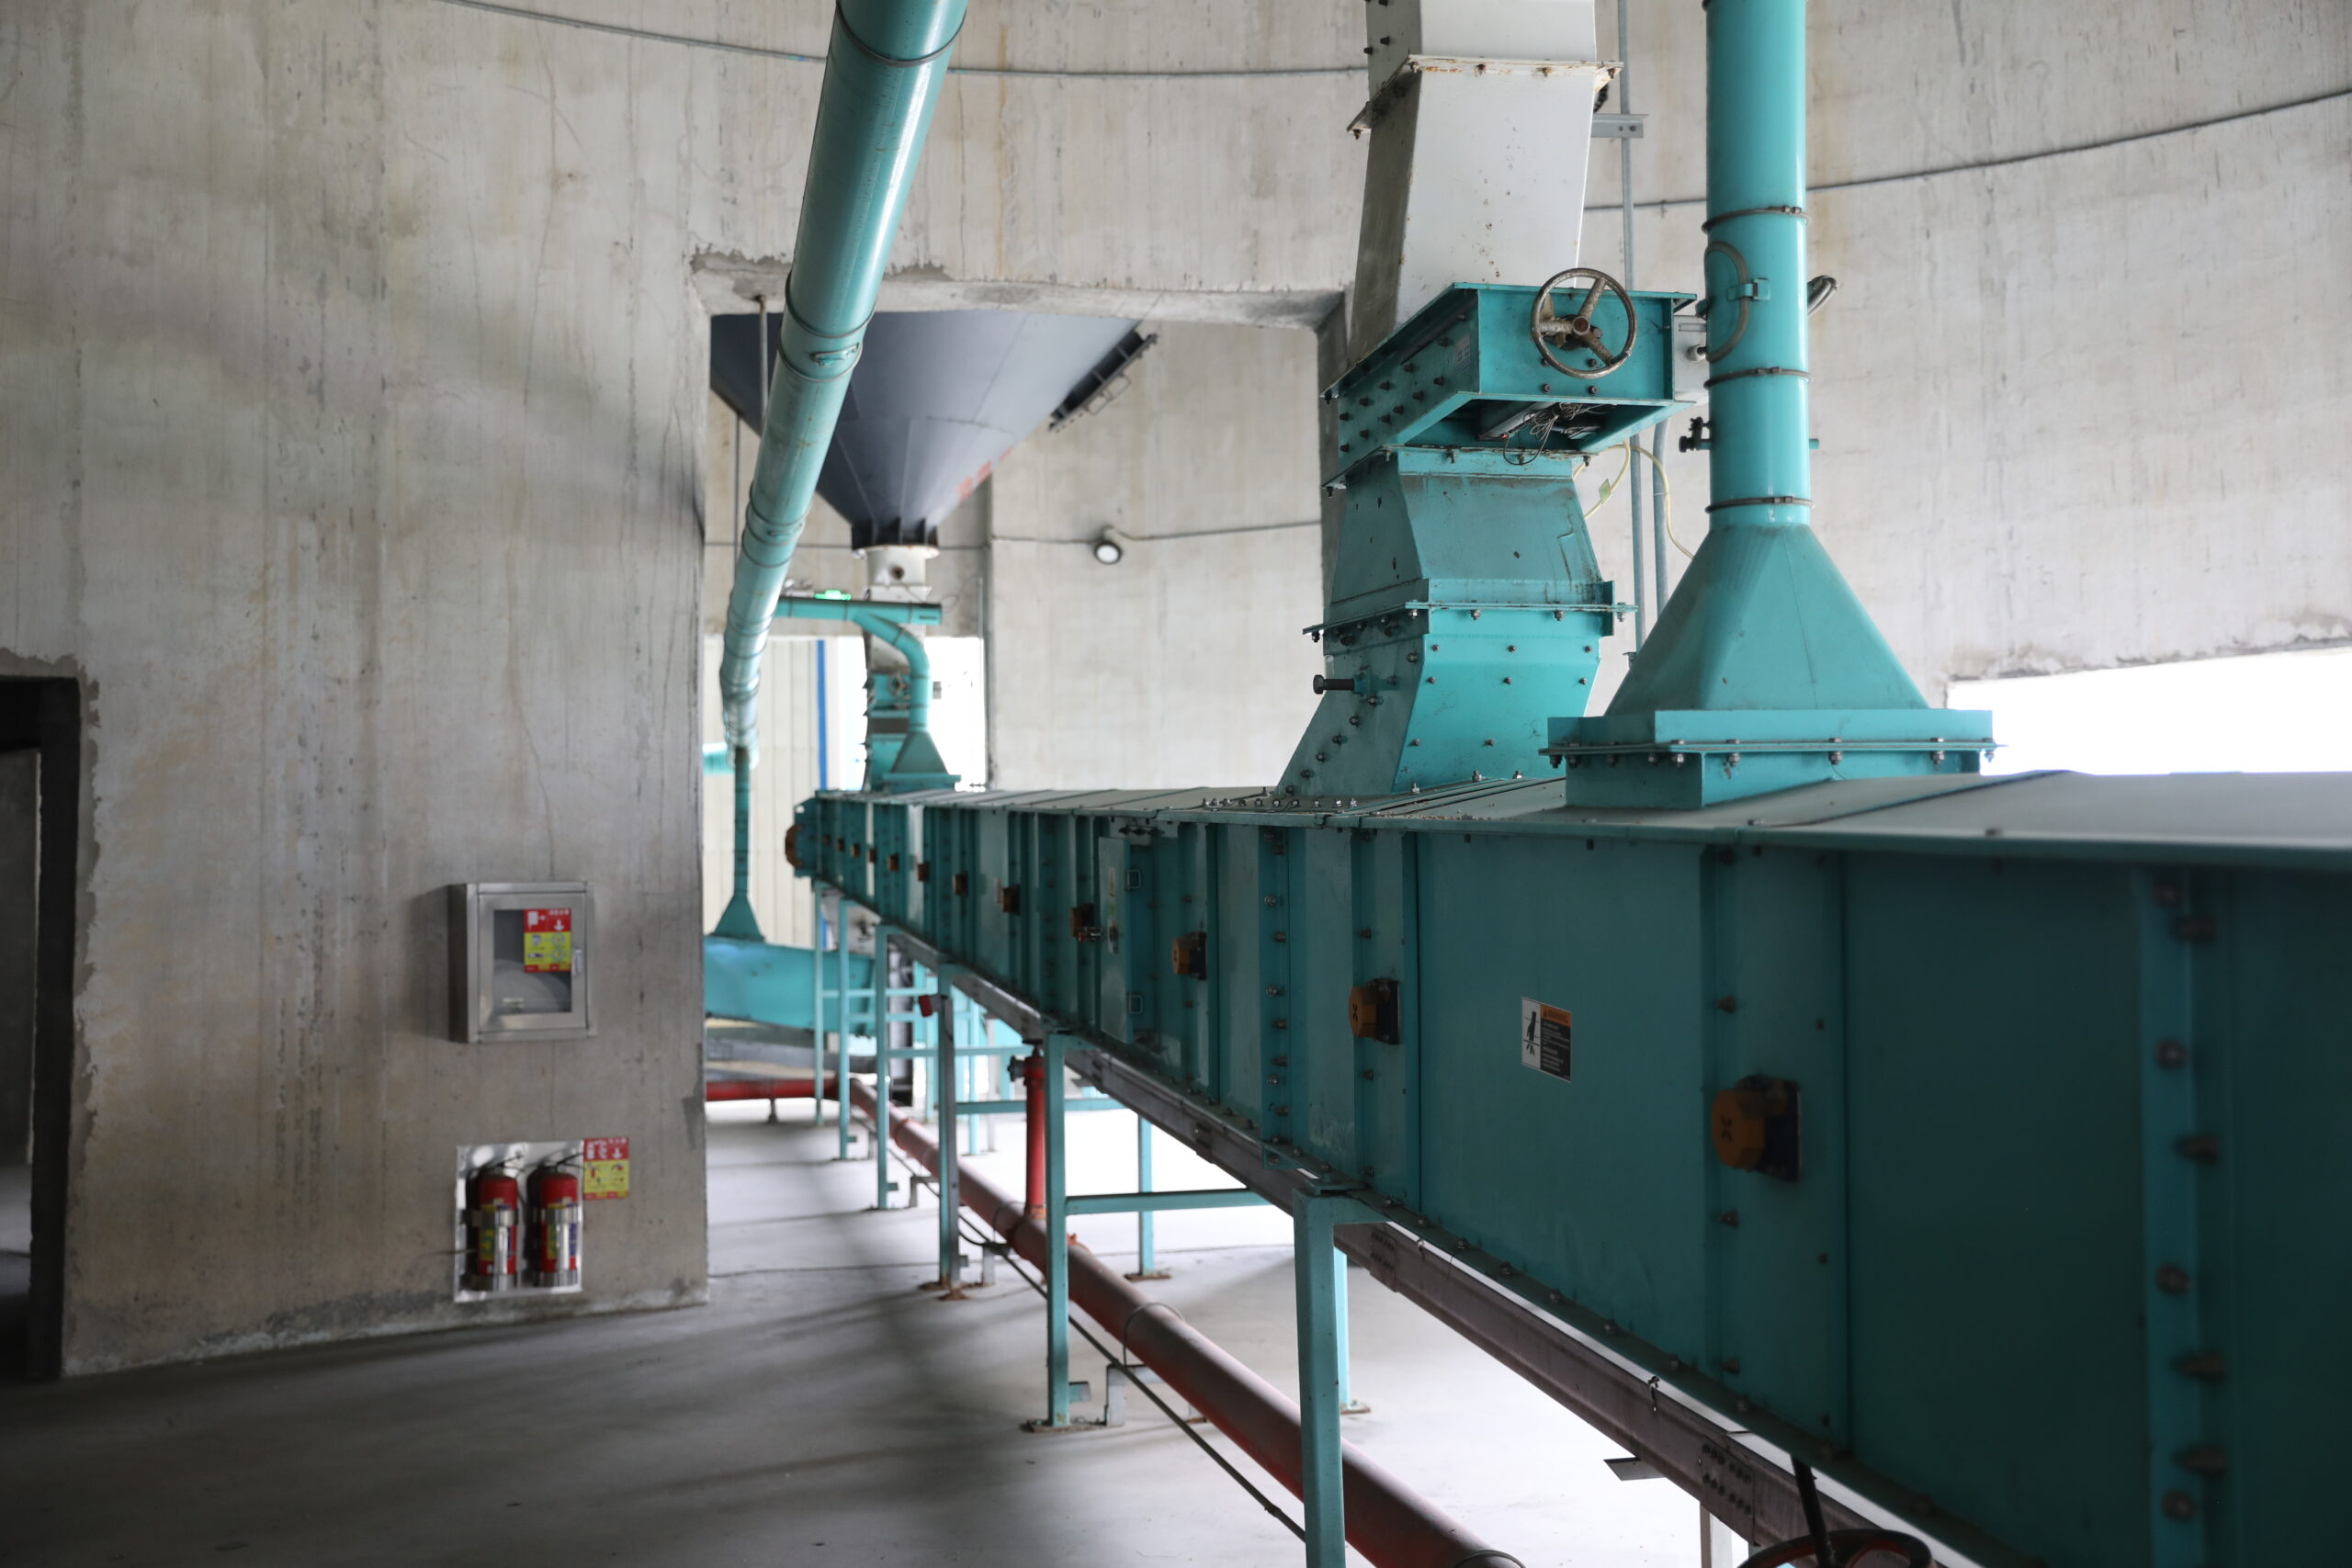
Deployed a complete GSS automated handling system specifically engineered for processing wheat. The equipment package includes 4 units of GSS 500 t/h air-supported belt conveyors (totaling 1.4 km in length), 8 units of GSS enclosed belt conveyors , 14 units of GSS en-masse conveyors , 6 units of GSS up-load drag conveyors , and 1 unit of bucket elevator .
Overcame the 1.4 km long-distance transfer barrier to enable seamless dock-to-plant automated delivery; air-cushion technology achieved dust-free, low-breakage transport protecting premium flour quality; weather-resistant construction ensured stable 24/7 coastal operation under high humidity and sea breezes.
Client Profile: A Major Port-Side Flour Processing Hub in East China
Located in a key coastal industrial bay in East China, the Yihai Kerry Wenzhou (Wilmar Group) Port-Side Processing Base is a premier integrated food and agricultural complex. Equipped with a dedicated deep-water berth handling 4.5 million tons annually, the facility integrates ocean grain vessel unloading, silo storage, and high-end flour processing, serving as a vital strategic logistics and manufacturing hub in the region.
Goals & Challenges: 1.4 km Long-Distance Transport & Zero-Dust Premium Grain Standards
As a large-scale port-side flour processing base, the facility faced several universal industry challenges during grain receiving and interterminal transfer:
- 1.4 km Ultra-Long Distance Conveying Bottleneck: Transferring wheat from dockside unloaders across 1.4 km to processing workshops required high-capacity (500 t/h) continuous equipment that eliminated high friction energy losses, material spillage, and intermediate re-handling.
- Dust-Free Handling & Premium Flour Quality Protection: High-grade flour milling demands absolute cleanliness, minimal grain breakage, and zero dust contamination during high-speed wheat intake.
- Coastal Environment Resistance & 24/7 Duty: Operating in a coastal environment exposes equipment to sea breezes and extreme humidity, requiring high corrosion resistance and mechanical stability for uninterrupted 24/7 service.
GSS Customized Solution: 1.4 km Air-Supported Conveying & Silo Storage Package
To satisfy Wilmar’s complex operational and quality standards, GSS delivered a customized bulk material handling package specifically engineered for processing wheat:
- 1.4 km Air-Supported Belt Conveyor System: Deployed 4 units of 500 t/h air-supported belt conveyors (lengths: 181.7 m, 511 m, 265.3 m, and 416.2 m; total distance approx. 1.4 km). Operating on an air cushion, this system dramatically reduces friction, eliminates material spillage, prevents dust escape, and cuts power consumption for long-distance transport.
- Wheat Silo Storage & Transfer System: Deployed 1 unit of 200 t/h bucket elevator (20 m lift height), 8 units of enclosed belt conveyors (1 unit at 500 t/h / 55 m length, and 7 units at 200 t/h with lengths up to 77.9 m), 14 units of en-masse conveyors (2 units at 500 t/h, and 12 units at 200 t/h), and 6 units of up-load drag conveyors (2 units at 100 t/h, and 4 units at 200 t/h with lengths up to 38.8 m).
Project Value
Integrated Logistics
The GSS 1.4 km air-supported conveying system eliminated intermediate truck re-handling, achieving seamless dock-to-plant automated delivery and significantly reducing logistics costs.
Dust-Free Transport
Air-cushion suspension reduced friction and grain breakage, maintaining wheat integrity and cleanliness from intake to milling, perfectly supporting high-end flour processing standards.
Cost Reduction
Heavy-duty, weather-resistant GSS equipment provided stable service under harsh coastal conditions, reducing power consumption and maintenance requirements.
"Operating a premier port-side flour processing complex requires a conveying system that combines long-distance capability with strict dust control. The complete bulk handling solution provided by GSS has delivered exceptional performance. The 1.4 km air-supported belt conveyors handle wheat intake from dock to plant effortlessly with low power consumption and zero spillage. GSS has provided reliable technical support for our high-capacity, automated flour base."