Low-Breakage Enclosed Conveying System | Luhua Group Premium Rice Milling Base
Key Highlights
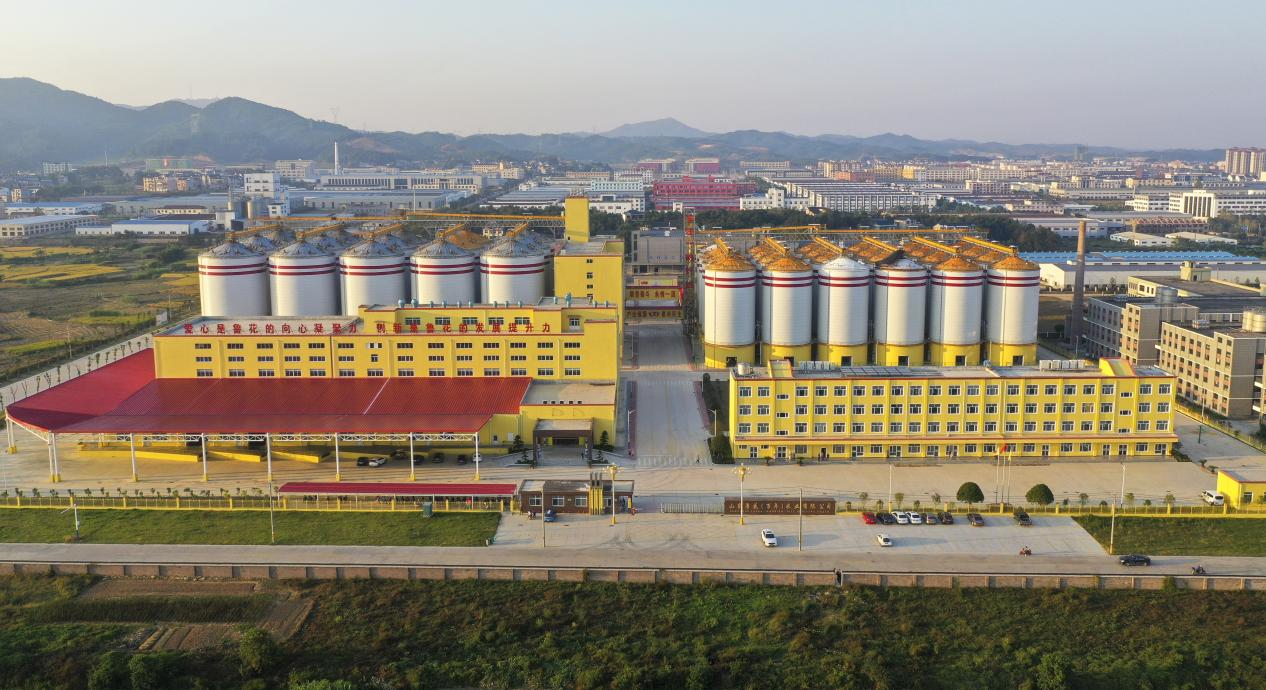
Luhua Rice (a major subsidiary of Luhua Group), operating a flagship modern premium rice milling complex in East China, required a high-reliability, dust-tight, and low-breakage outdoor bulk conveying system for its large-scale paddy processing lines.
GSS deployed a complete automated bulk conveying system specifically engineered for processing paddy and handling separated impurities. The comprehensive equipment package includes 17 units of GSS paddy bucket elevators and 68 units of GSS en-masse conveyors.
Low grain breakage mechanics preserves premium rice quality and minimizes post-harvest losses; weatherproof, dust-tight enclosed construction ensures reliable 24/7 outdoor operation; optimized plant layout boosts automation while lowering maintenance costs.
Client Profile: A Premier Eco-Friendly Rice Processing Base in East China
Located in East China, Luhua Rice (Luhua Group) is a premier modern agricultural processing base under one of China’s top agricultural and edible oil market leaders. Focused on high-quality, eco-friendly rice milling and brand operations, the complex leverages rich local paddy resources to create an intelligent, low-loss, and ultra-clean production facility, setting a green manufacturing benchmark for regional grain processing.
Goals & Challenges: Outdoor All-Weather Transfer & Low-Breakage Premium Rice Standards
As a high-end eco-friendly rice processing complex, the facility faced several universal industry challenges during outdoor raw grain transfer and workshop feeding:
- Weatherproof Outdoor Transfer & All-Weather Reliability: Raw paddy transfer from storage silos to processing workshops takes place outdoors. Equipment must withstand moisture, rain, and temperature fluctuations without material clogging or mechanical breakdowns.
- Strict Low-Breakage Standards for Premium Rice: Luhua’s premium brand positioning demands strict control over rice breakage during handling. Additionally, dust-tight enclosures are required to prevent environmental pollution and grain spillage.
- Plant-Wide Process Optimization & Energy Efficiency: Connecting storage silos with processing lines requires a streamlined conveying layout to eliminate transfer bottlenecks, minimize manual intervention, and reduce operational energy costs.
Customized Solution: Plant-Wide Enclosed Conveying System
To satisfy Luhua Group’s strict quality and operational standards, GSS delivered a customized, full-process bulk material handling solution specifically engineered for processing paddy and handling separated impurities:
- GSS Low-Breakage Paddy Bucket Elevators (17 units) : Deployed 17 units of bucket elevators, including 16 units at 120 t/h capacity (lift heights ranging from 10.1m to 41.8m) and 1 unit at 50 t/h capacity (32.5m lift height). Engineered with gentle inlet and discharge mechanics, these elevators perform reliable vertical elevation with minimal grain breakage.
- GSS Dust-Tight En-Masse Conveyors for Paddy & Impurities (68 units): Deployed 68 units of en-masse conveyors, featuring 62 units at 120 t/h capacity for paddy (lengths up to 54m), 1 unit at 50 t/h capacity for paddy, and 5 units at 2 t/h capacity for dust and impurity removal. Built with dust-tight enclosures and wear-resistant flights, these units ensure clean, uninterrupted horizontal transfer across outdoor and indoor workshop lines.
- Tailored Plant Layout & Weatherproof Design:Customized conveyor routes seamlessly bridge outdoor storage silos and indoor processing lines, optimizing transfer paths, preventing moisture intake, and ensuring smooth closed-loop material flow.
Project Value
for All-Weather Transfer
The robust, dust-tight design of GSS bucket elevators and en-masse conveyors effectively eliminates moisture intrusion and dust leakage, ensuring seamless raw grain transfer under outdoor conditions.
Low-Breakage Transport
Gentle conveying mechanics reduces paddy breakage, protecting original grain quality and supporting Luhua’s high brand standards for premium eco-friendly rice.
Lowering Operating & Energy Costs
Optimized conveying paths and low-failure GSS equipment minimizes manual intervention and maintenance expenses, aligning perfectly with green smart factory standards.
"Producing high-end eco-friendly rice requires uncompromised quality control across all material handling stages. The complete conveying system provided by GSS has performed exceptionally well under our outdoor transfer conditions. Its 17 bucket elevators and 68 en-masse conveyors deliver smooth, dust-tight, and low-breakage paddy transport between our storage silos and milling lines. GSS has provided reliable technical support for our green, premium rice processing facility."