Multi-Material Heavy-Duty Conveying System | Yihai Kerry Zhoukou 1Mt Corn Processing Hub
Key Highlights
Yihai Kerry Zhoukou (Wilmar Group), operating a flagship 1-million-ton annual capacity corn processing hub in Central China, urgently required an integrated, heavy-duty bulk handling system for corn intake, starch processing, oil extraction, and by-product recycling.
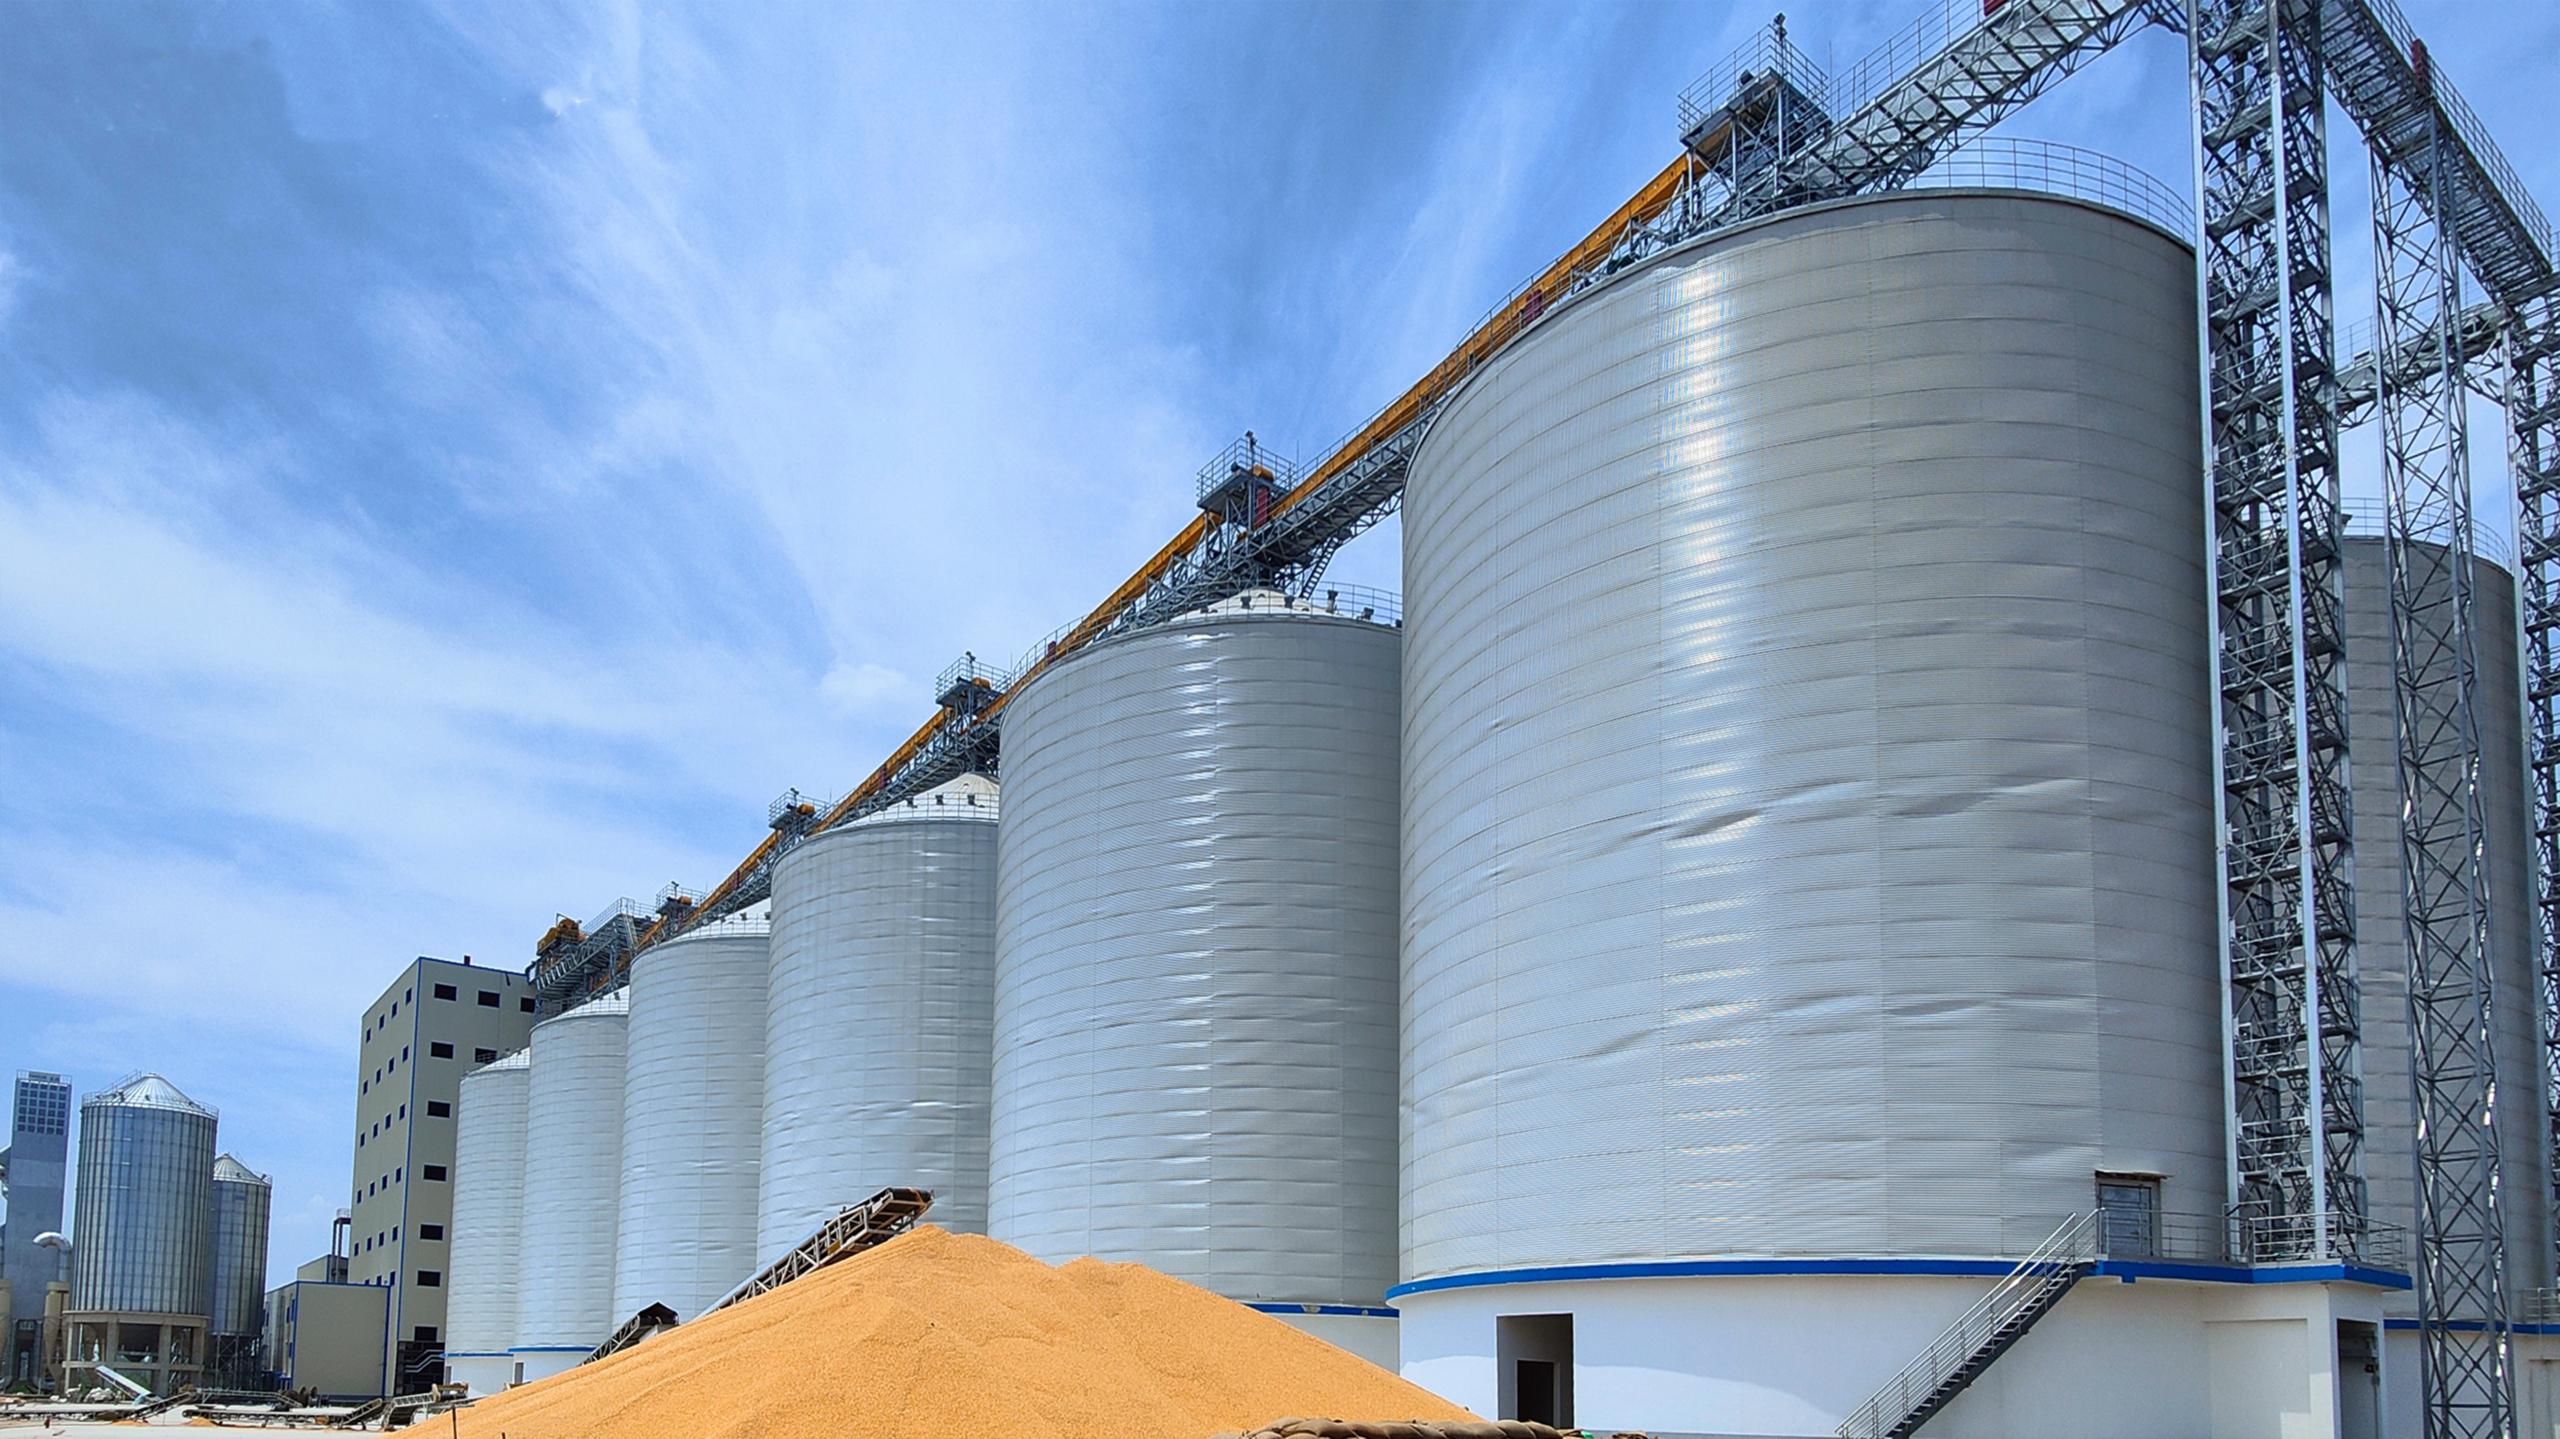
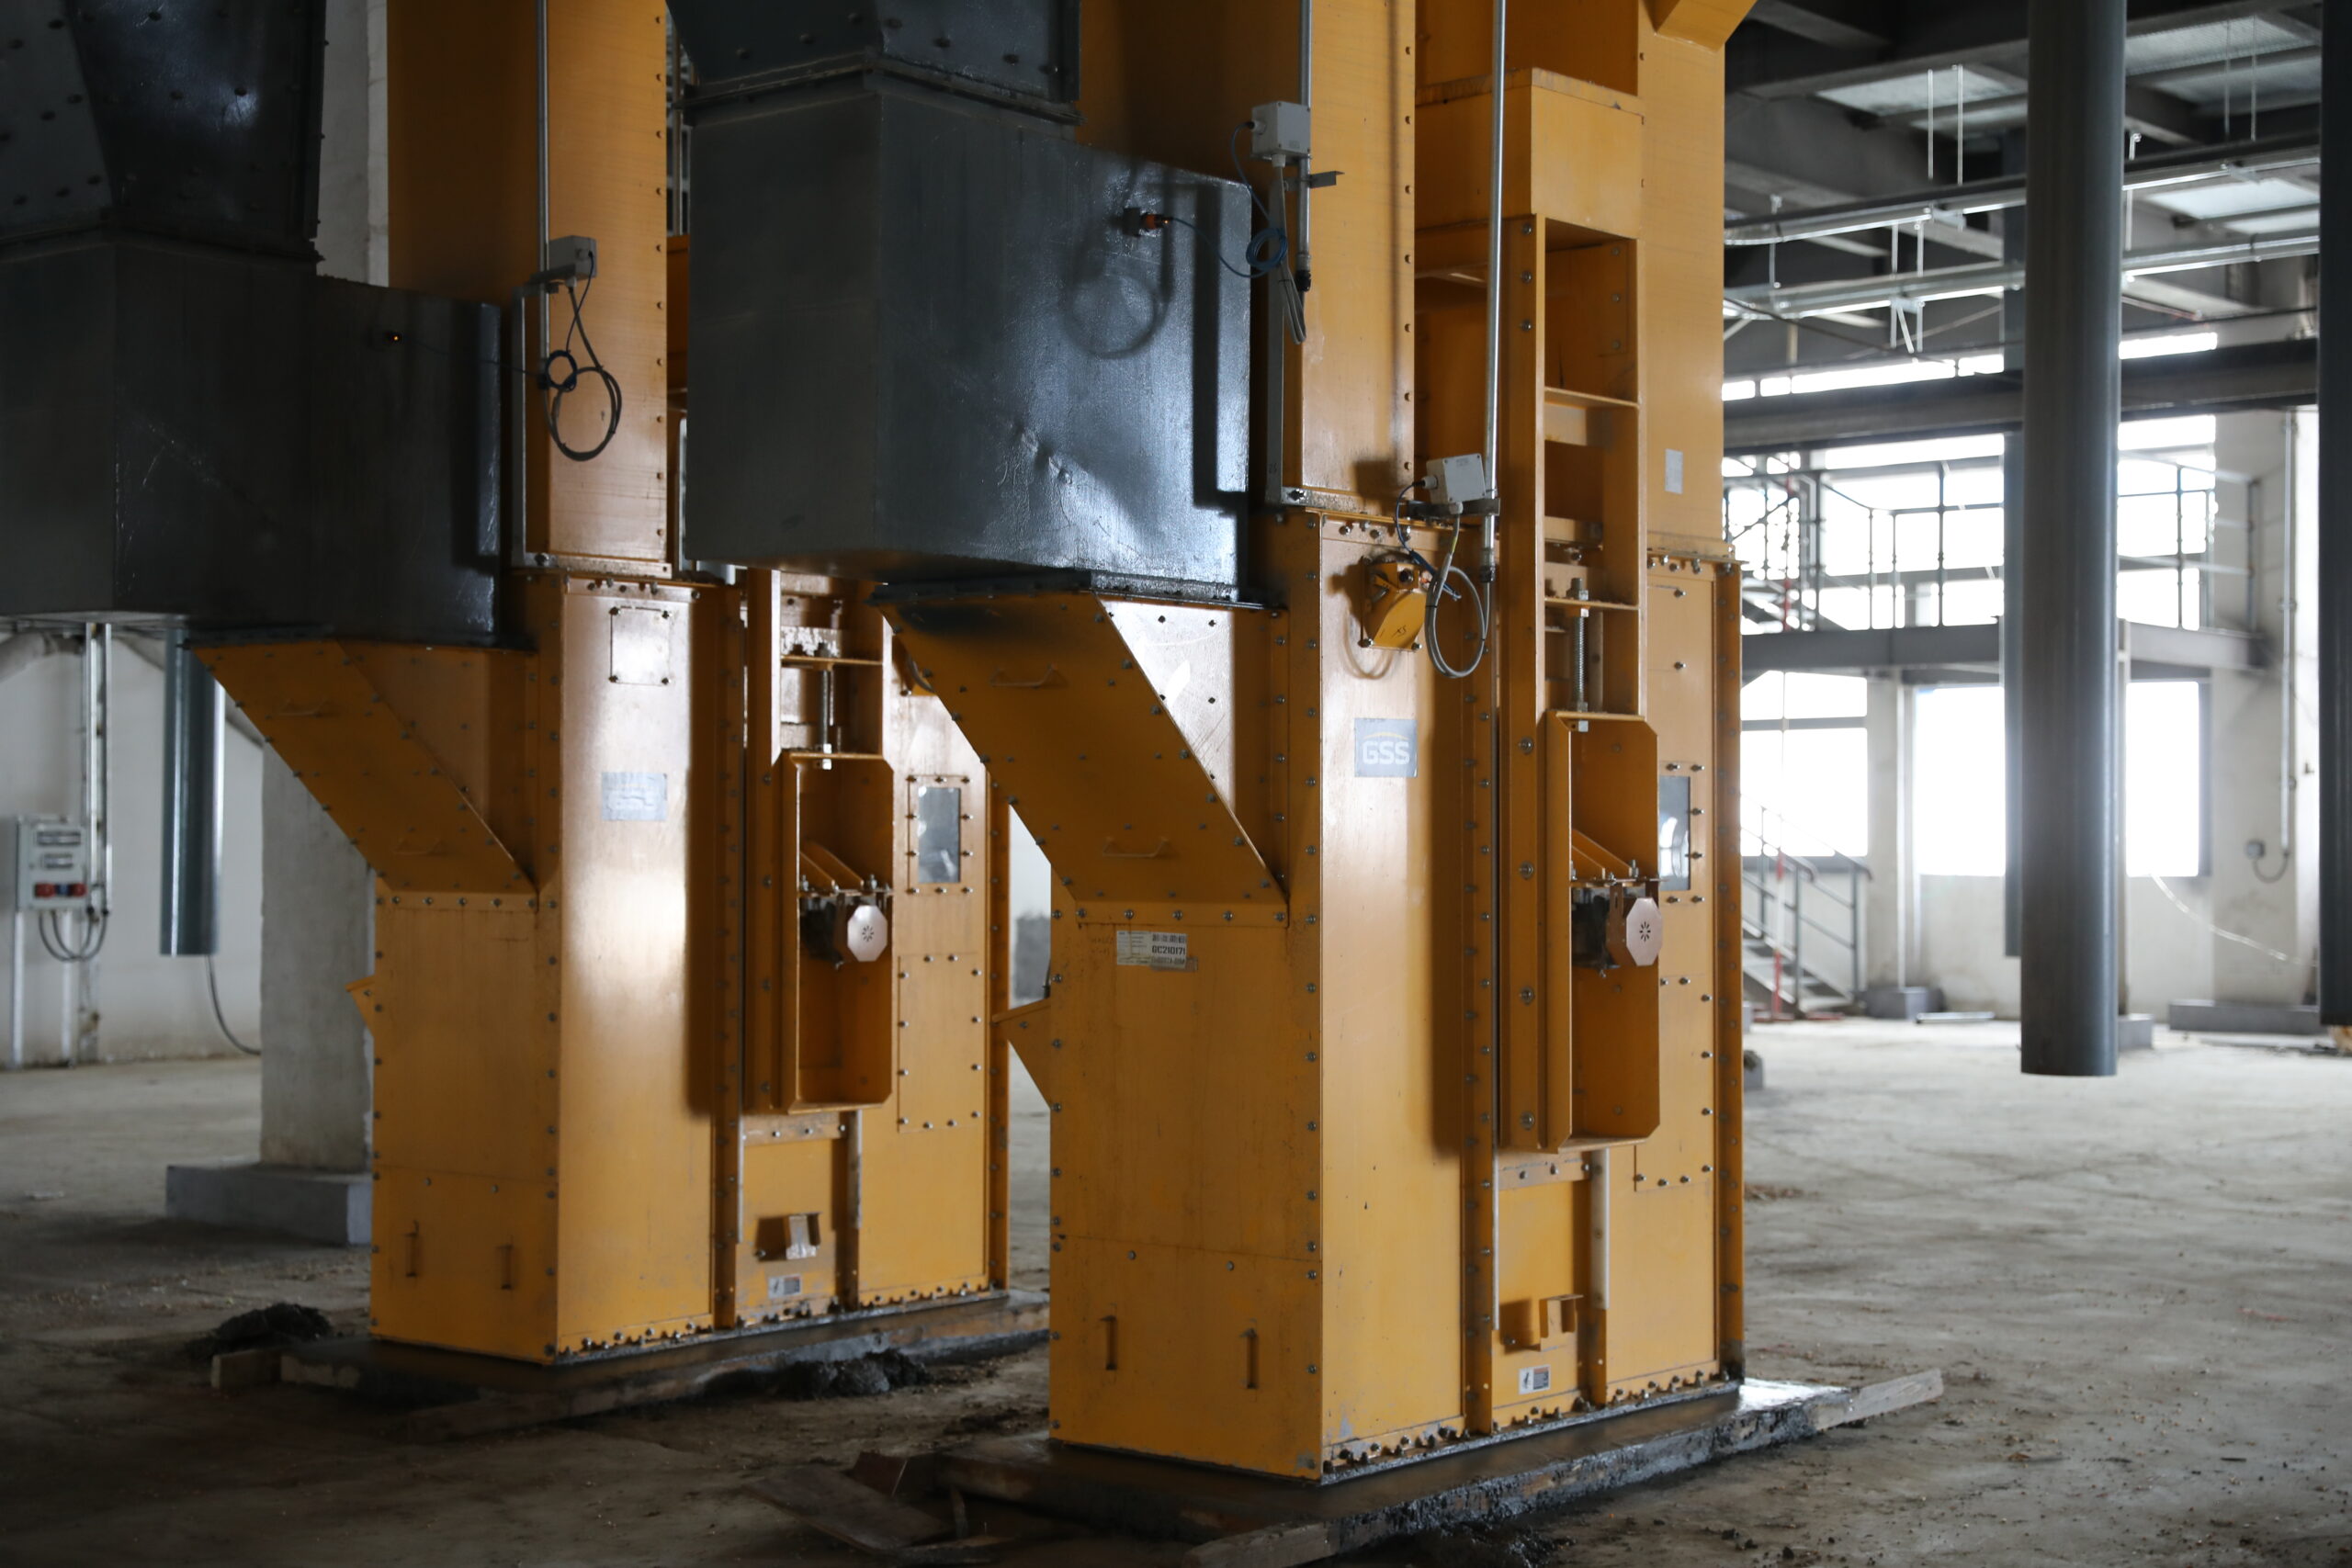
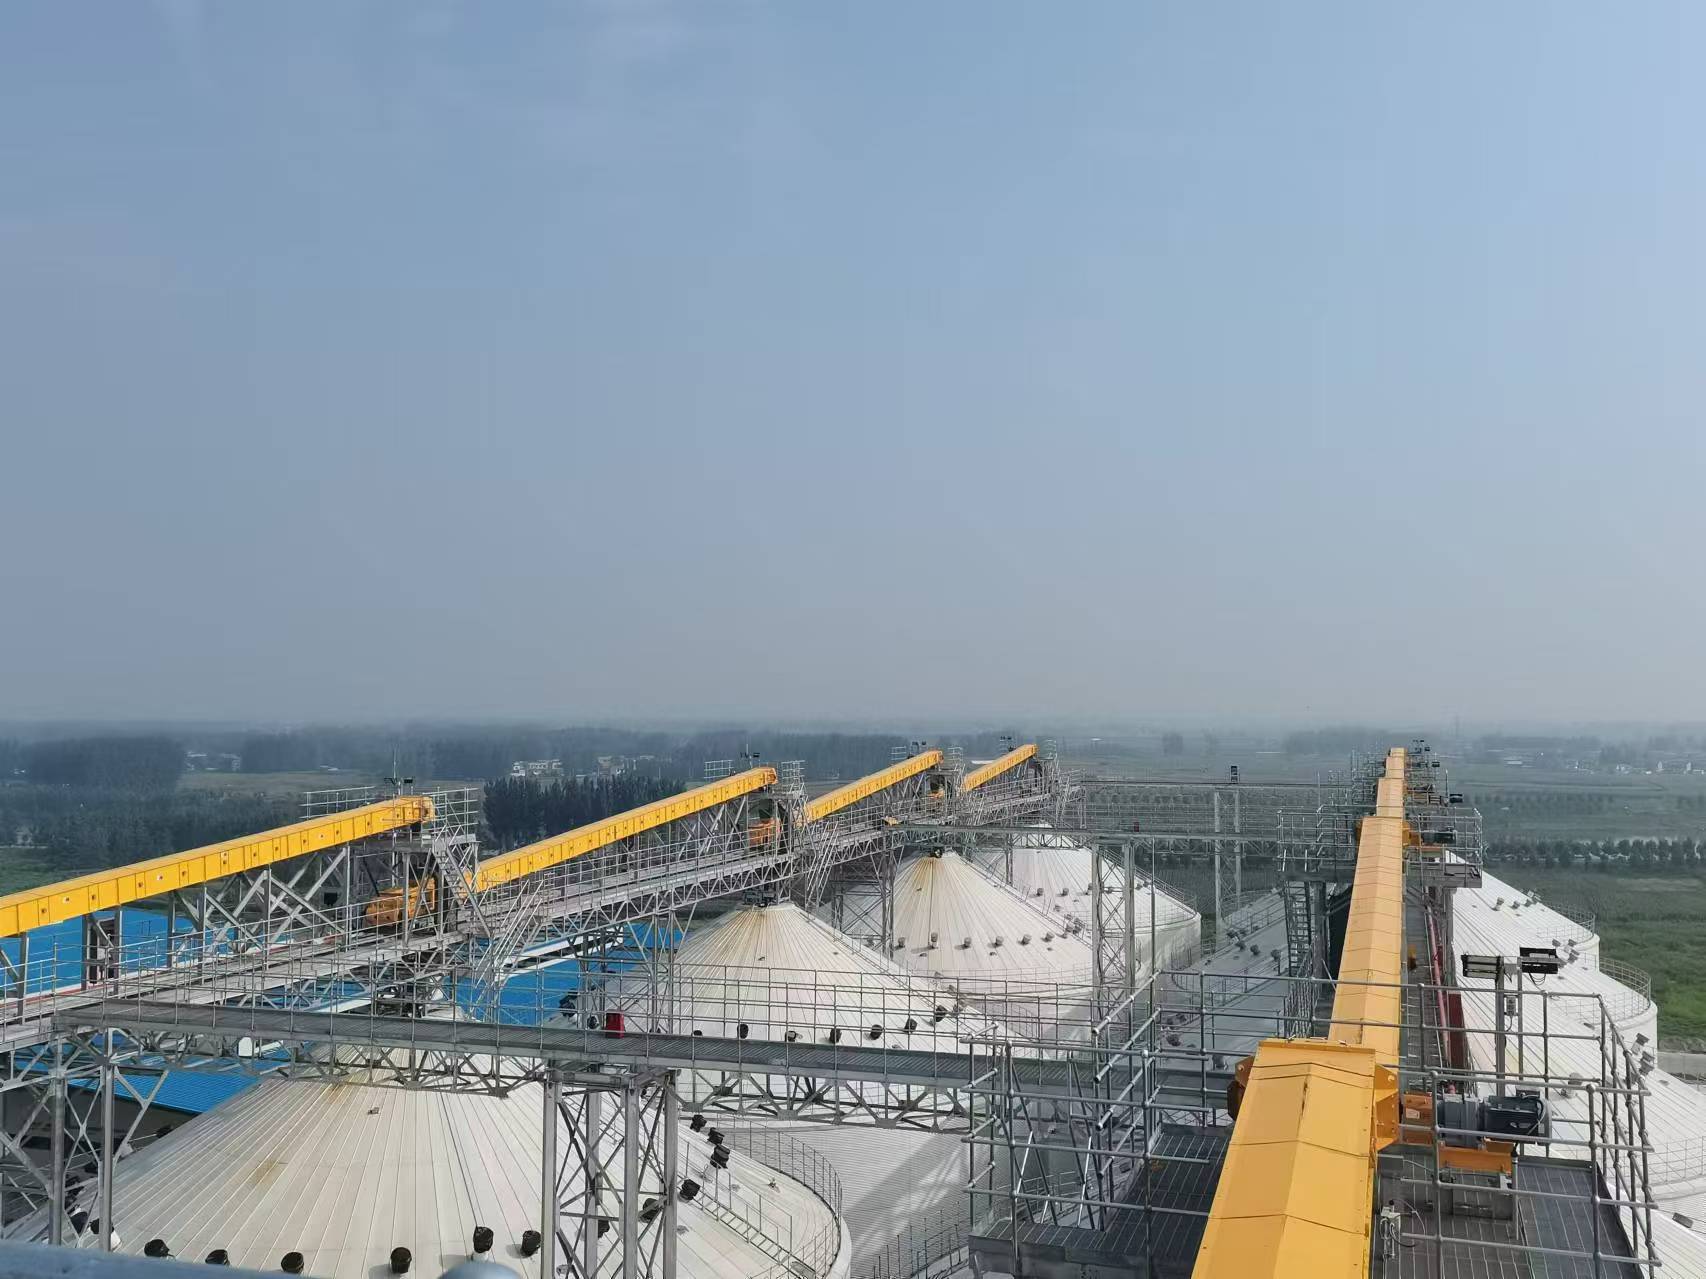
GSS deployed a fully automated bulk conveying system custom-designed for raw corn, corn germ, corn germ cake, corn germ meal and extruded corn. The scope covers 5 raw corn bucket elevators, 7 up-load drag conveyors, 17 enclosed belt conveyors, 3 by-product en-masse conveyors and 2 screw conveyors.
The 300 t/h high-throughput intake lines seamlessly supported 1-million-ton annual processing goals; steep-incline up-load drag conveyors (up to 70°) solved tight workshop space limits; dust-tight enclosures and low-breakage designs maximized byproduct economic value and satisfied green factory standards.
Client Profile: A 1-Million-Ton Corn Processing Base in Central China
Located in a key inland port logistics zone in Central China, the Yihai Kerry (Wilmar Group) Biotech Complex is a flagship mega-scale agricultural deep-processing center. Designed with an annual processing capacity of 1 million tons of corn, the complex integrates corn starch processing, oil extraction, and bio-manufacturing, achieving a zero-waste, circular economy model for agricultural resources.
Goals & Challenges: Multi-Material Handling & High-Incline Space Constraints
As a mega-scale corn processing hub, the facility faced several universal industry challenges across its raw grain intake and byproduct lines:
- High-Volume Raw Corn Intake (300 t/h): The facility needed high-capacity intake conveying lines capable of 300 t/h continuous throughput to rapidly unload incoming trucks, elevate material into silos, and feed processing workshops without bottlenecks.
- Handling Diverse & Difficult Byproducts: Oil extraction byproducts vary significantly in moisture, density, and stickiness. Equipment must smoothly transport powdery, granular, and semi-adhesive materials without choking or residue buildup.
- Steep Incline Space Limits & Dust Control: Compact workshop layouts required steep-inclined elevation (up to 70° incline) for byproduct transfer, alongside dust-tight enclosures to meet environmental standards.
Customized Solution
To satisfy Wilmar’s multi-material operational and environmental standards, GSS delivered a customized, full-process bulk handling solution specifically engineered for raw corn and its processed byproducts:
- Raw Corn Silo Intake System (300 t/h): Deployed 5 units of 300 t/h raw corn bucket elevators (lift heights up to 56.5m), 3 units of 300 t/h up-load drag conveyors (45° and 60° inclines, lengths up to 54.7m) for pit unloading, and 17 units of 300 t/h enclosed belt conveyors (lengths up to 100m) for top-silo grain distribution.
- Specialized Byproduct Handling Package: Deployed 4 units of steep up-load drag conveyors customized for germ (25 t/h, 50° incline, 40m), germ cake (20 t/h, 70° incline, 29.3m), germ meal (15 t/h, 36° incline, 47.2m), and extruded corn (20 t/h, 34° incline, 37.4m); paired with 3 units of en-masse conveyors and 2 units of screw conveyors (15 t/h and 25 t/h).
- Full-Enclosure & Wear-Resistant Engineering: All equipment features dust-tight casings, wear-resistant liners, and low-breakage flight designs to prevent spillage, minimize material degradation, and maintain 24/7 continuous operation.
Project Value
Silo-to-Production Connectivity
GSS raw corn intake lines and byproduct handling systems seamlessly linked storage silos with starch and oil extraction lines, supporting uninterrupted 24/7 production.
Overcoming Space Limits
GSS up-load drag conveyors with inclines up to 70° efficiently elevated semi-adhesive and powdery byproducts in tight workshop quarters, eliminating choking and space constraints.
Environmental & Low-Breakage Operation
Full-enclosure designs and low-breakage conveying minimized raw material and byproduct losses, creating a clean working environment in line with circular bio-economy standards.
"Operating a 1-million-ton corn biotech complex requires conveying equipment that combines high intake capacity with extreme flexibility for handling diverse byproducts. The complete bulk handling solution provided by GSS has performed remarkably well across our raw corn silos and oil extraction lines. Its 300 t/h intake conveyors handle high-volume arrival effortlessly, while the steep-incline up-load drag conveyors deliver reliable, dust-tight transport for sticky germ cake and meal. GSS has provided solid equipment backing for our green, circular bio-manufacturing base."